thyssenkrupp RollSizer DRS

ANRANST manufactures and supplies RollSizer tooth plates (segments) through a complete process control chain; this page also keeps legacy model, dimension and spare identification. The former Mining Technologies business became part of FLS in 2022.

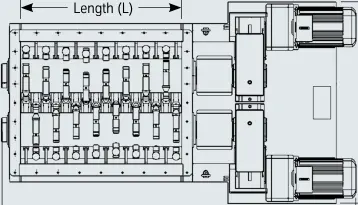
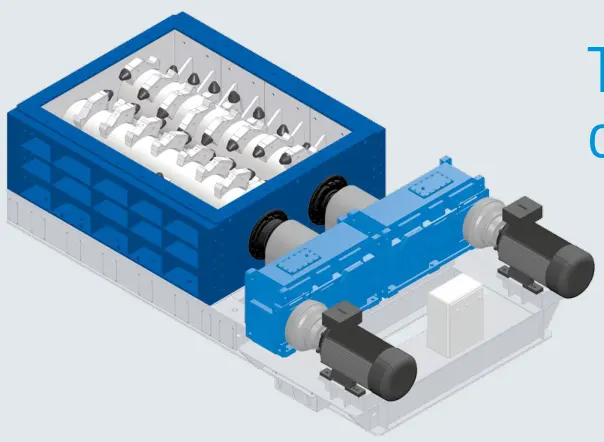
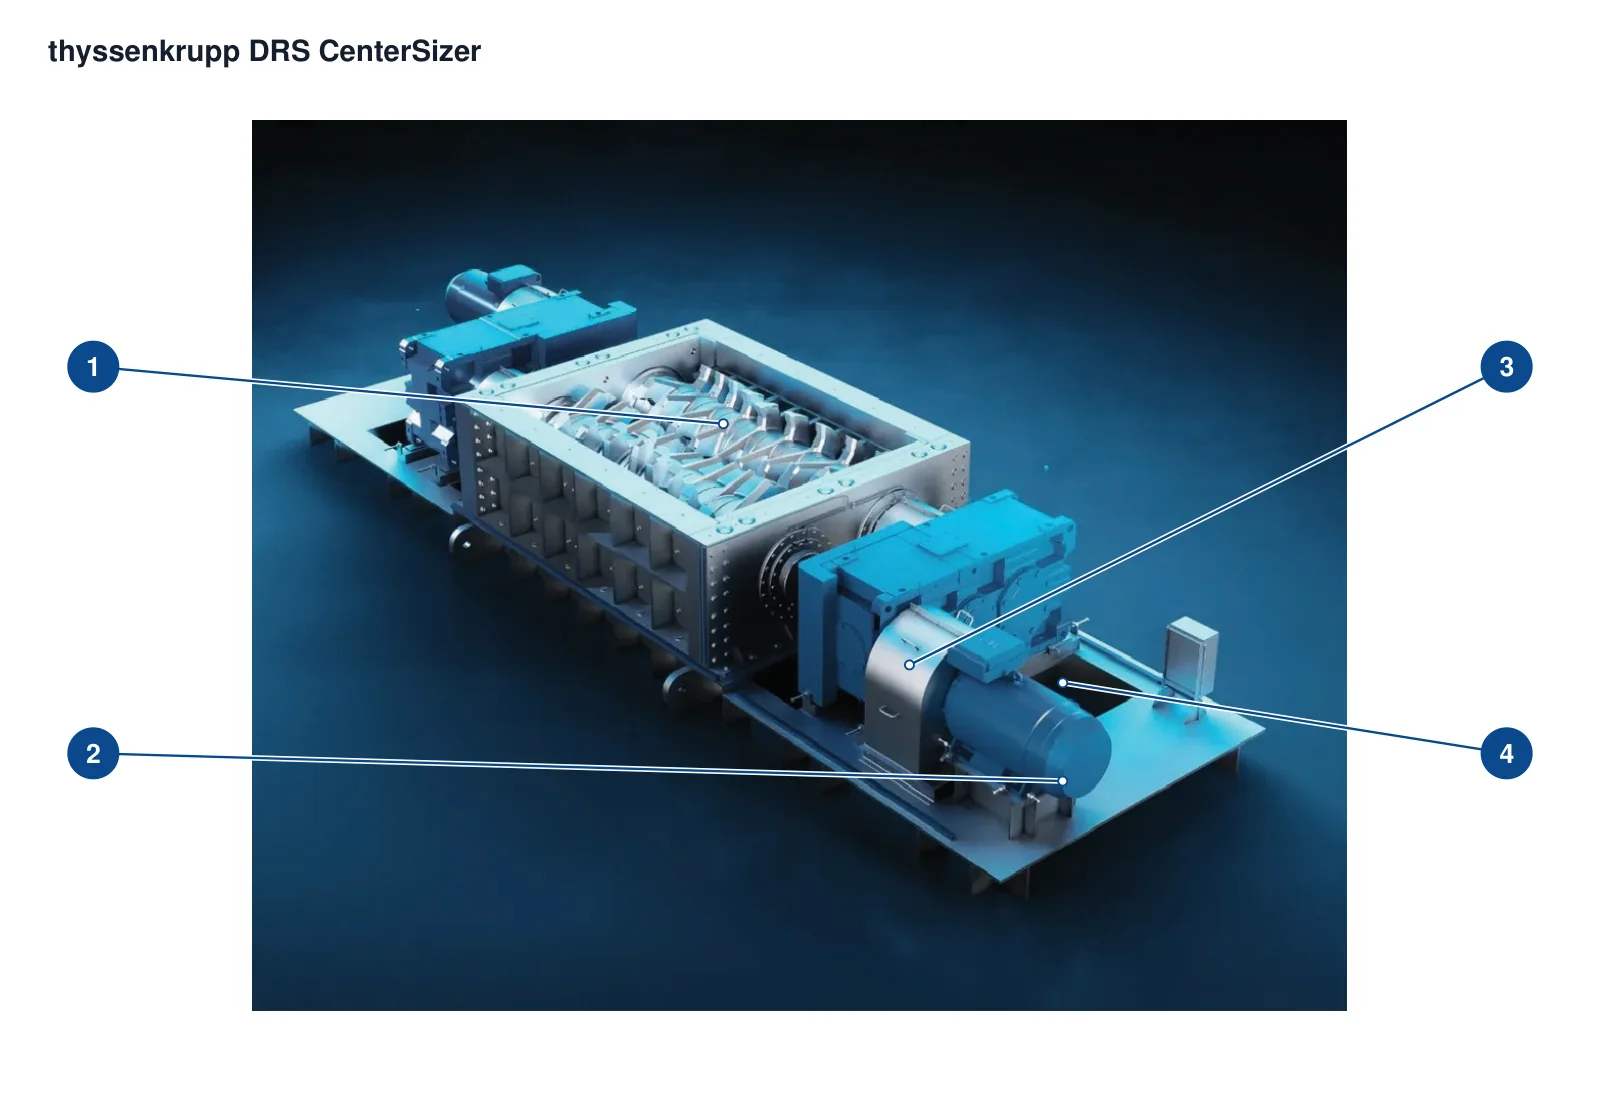
DRS 1000 × 3000 C (B) CenterSizer from an archived OEM data sheet, showing twin drives, housing and toothed rolls.
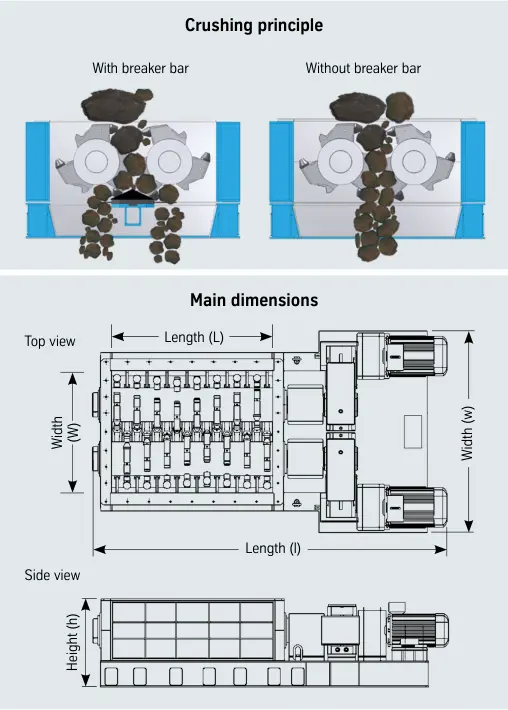
Archived OEM working principles with and without a breaker bar, plus principal dimension views.
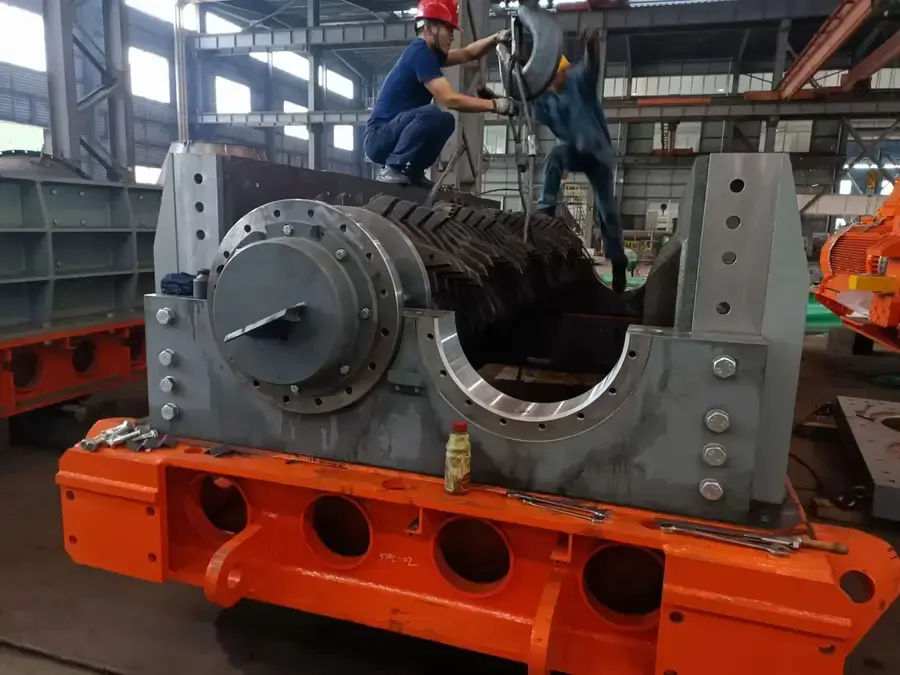
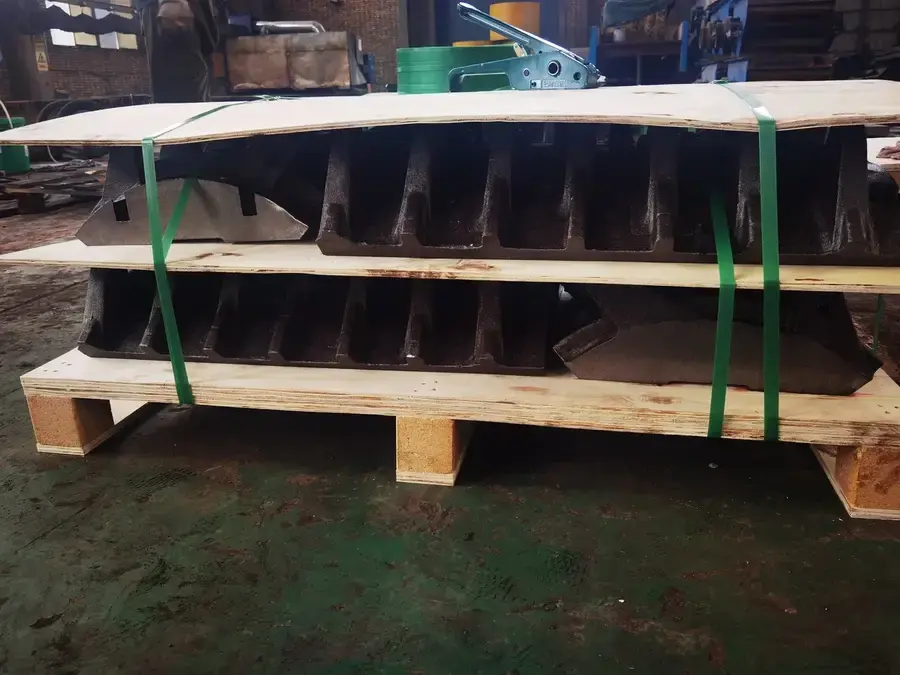
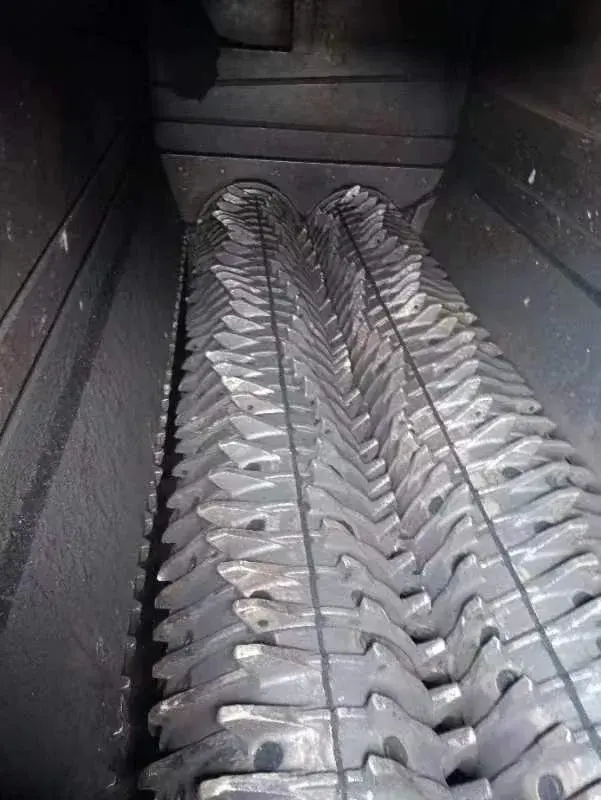
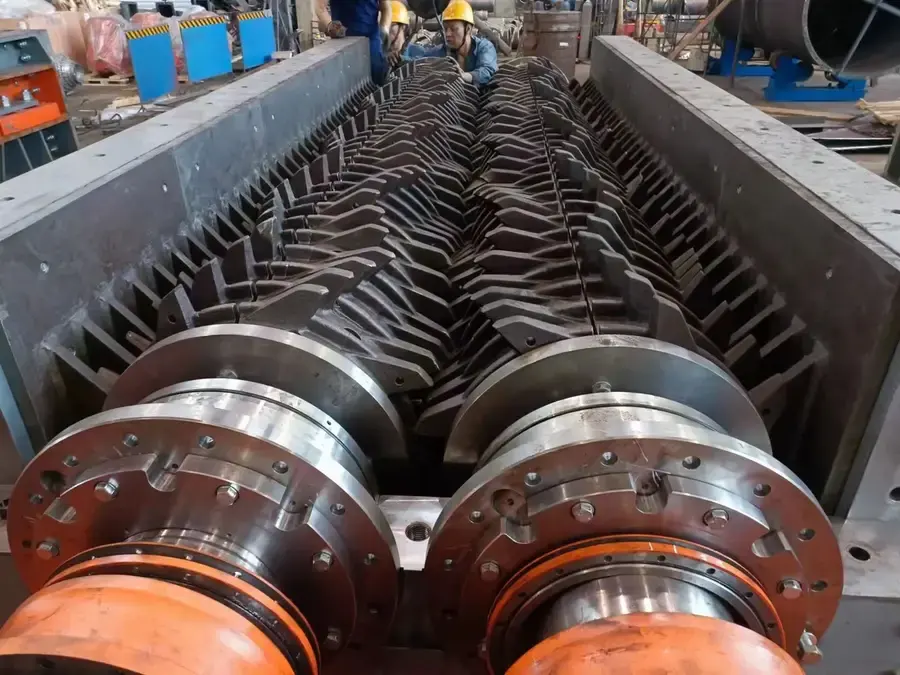
ANRANST archive photograph of tooth segments fitted to a similar twin-roll sizer, illustrating tooth sequence and position. Actual fitment follows the original drawings.
OEM Equipment Reference

Tooth plates made to process, with legacy install identification retained

ANRANST manufactures RollSizer tooth plates (segments) through the full process from proofing to finished acceptance, with process gates and complete documentation—not a model catalogue alone. RollSizer applies shear and tension at low speed and high torque; CenterSizer crushes between the rolls; SideSizer crushes between roll teeth and side combs. This page also identifies legacy wear parts and spares; project configurations do not establish universal interchangeability.

DRS 500–1500Historical standard series range
2CenterSizer / SideSizer arrangements
≤ 10,000 t/hHighest example capacity in the historical brochure
2022Mining Technologies became part of FLS
Manufacturing process

Tooth plate manufacturing process

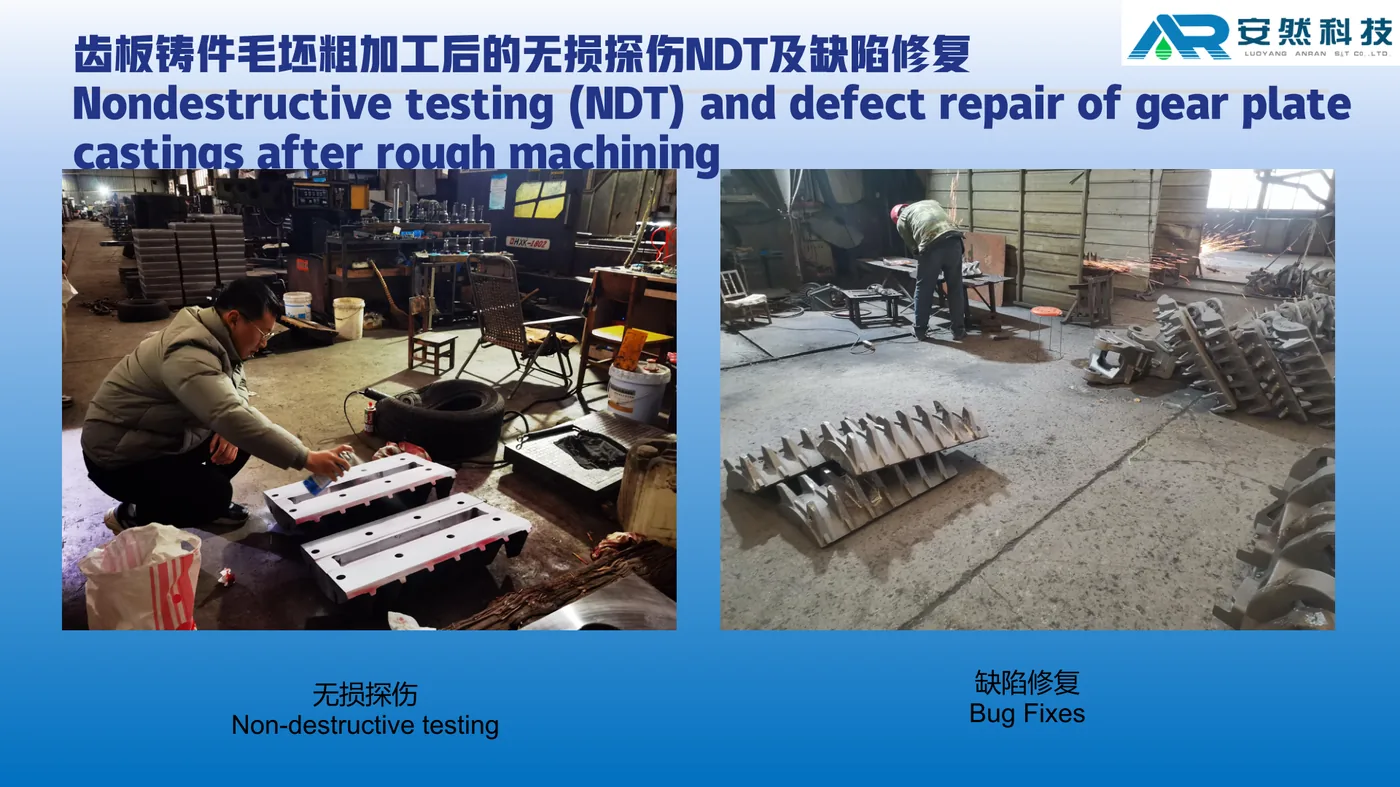
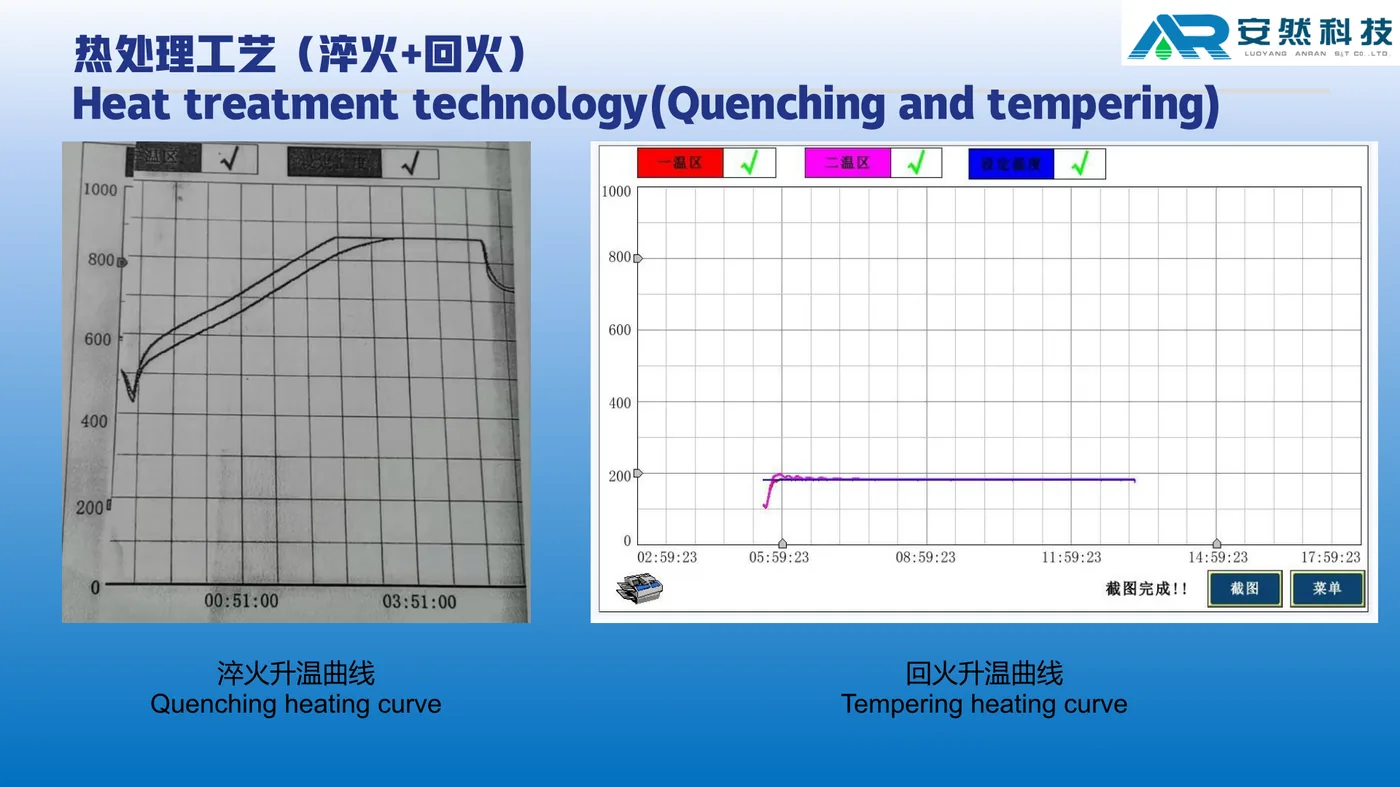
ANRANST manufactures and accepts RollSizer tooth plates (segments) through the full process below: early proofing and metal tooling, lost-foam shell making and firing, casting, cleaning and annealing, rough and finish machining, material-appropriate NDT and approved repair, heat treatment with hardness and toughness checks, then finished inspection, gauge fit and trial assembly. Steps are verifiable, inspection is traceable, and documents are kept complete; supply still follows the installed drawing, serial identity and duty conditions. Standard work, process records and open results are how process control is practiced—not empty management slogans.

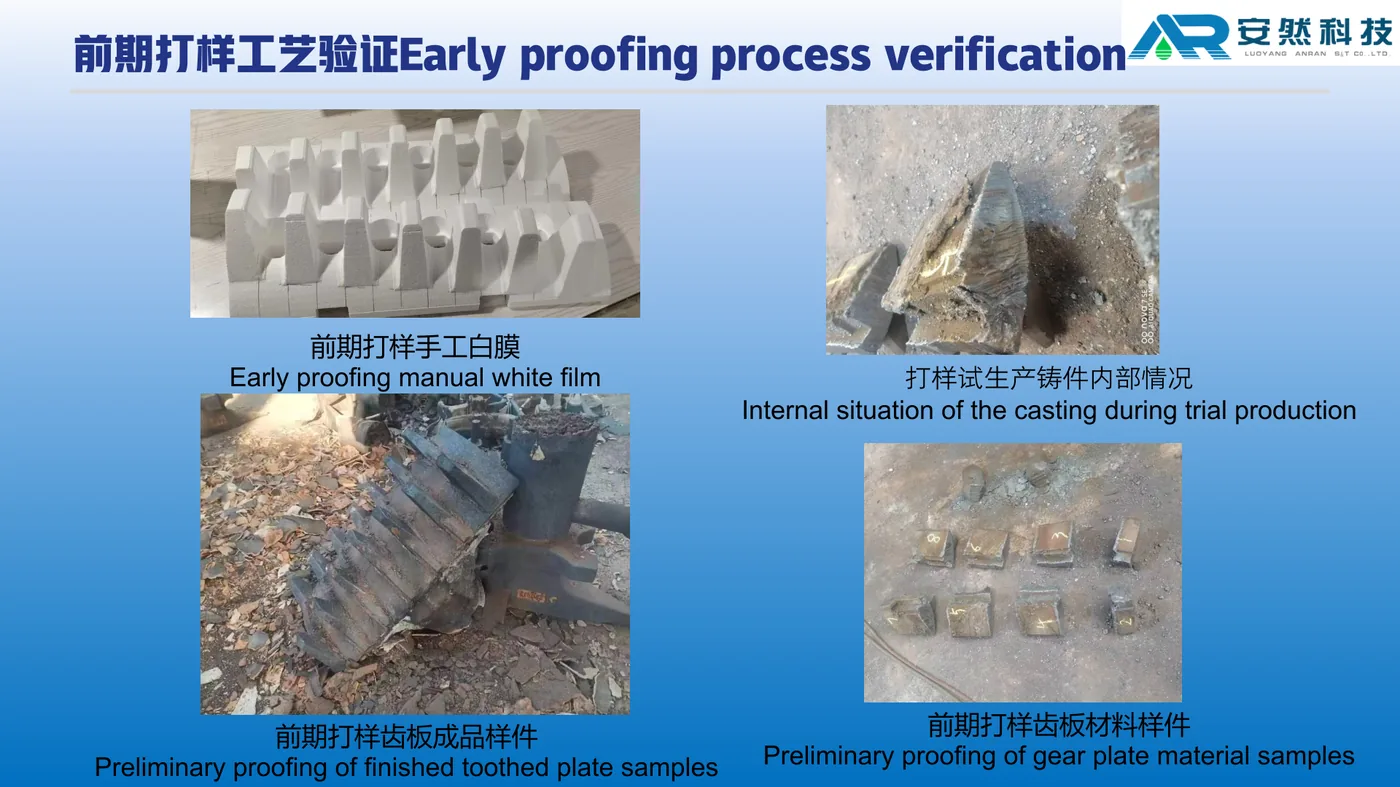
  1. Tooth plate process step 01: Early proofing process verification
    01Early proofing process verification前期打样工艺验证
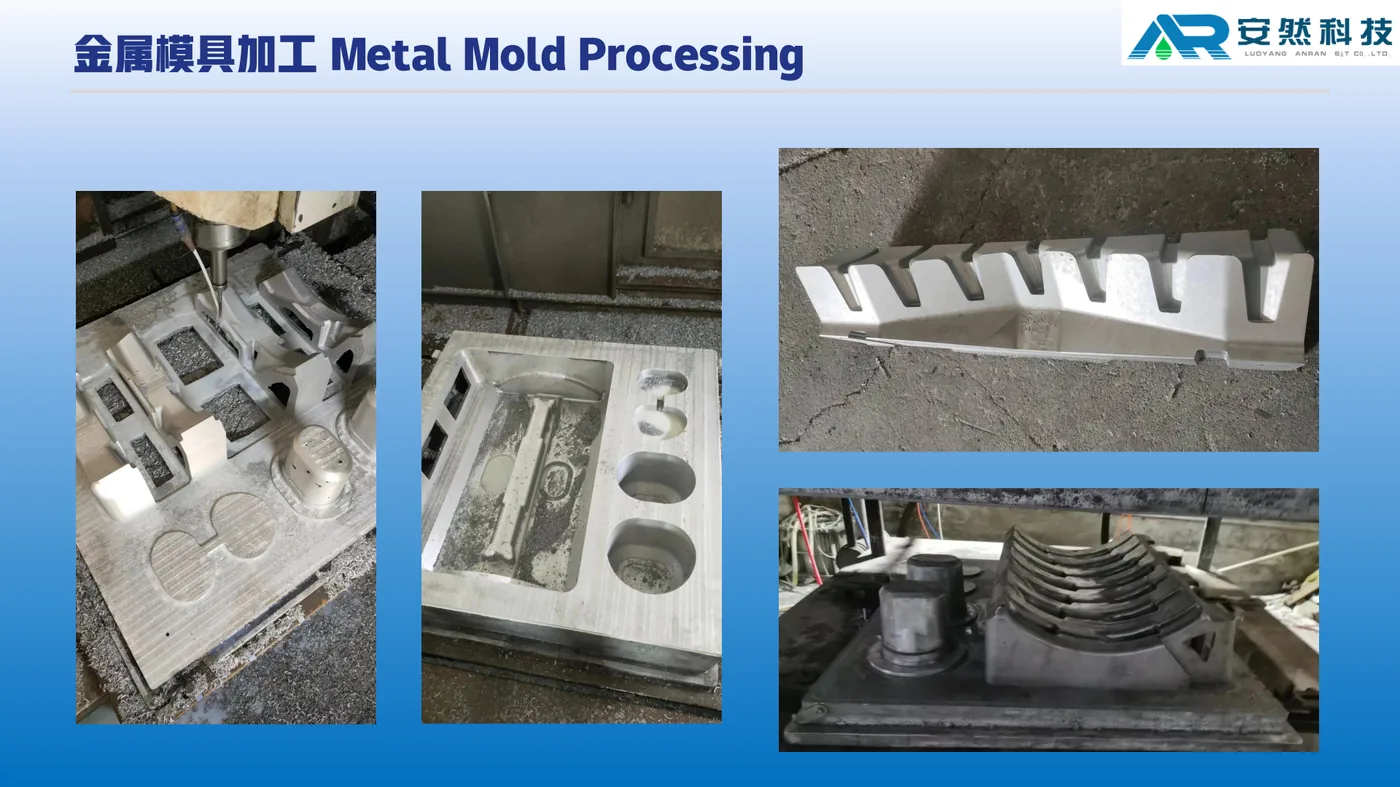
  2. Tooth plate process step 02: Metal mold processing
    02Metal mold processing金属模具加工
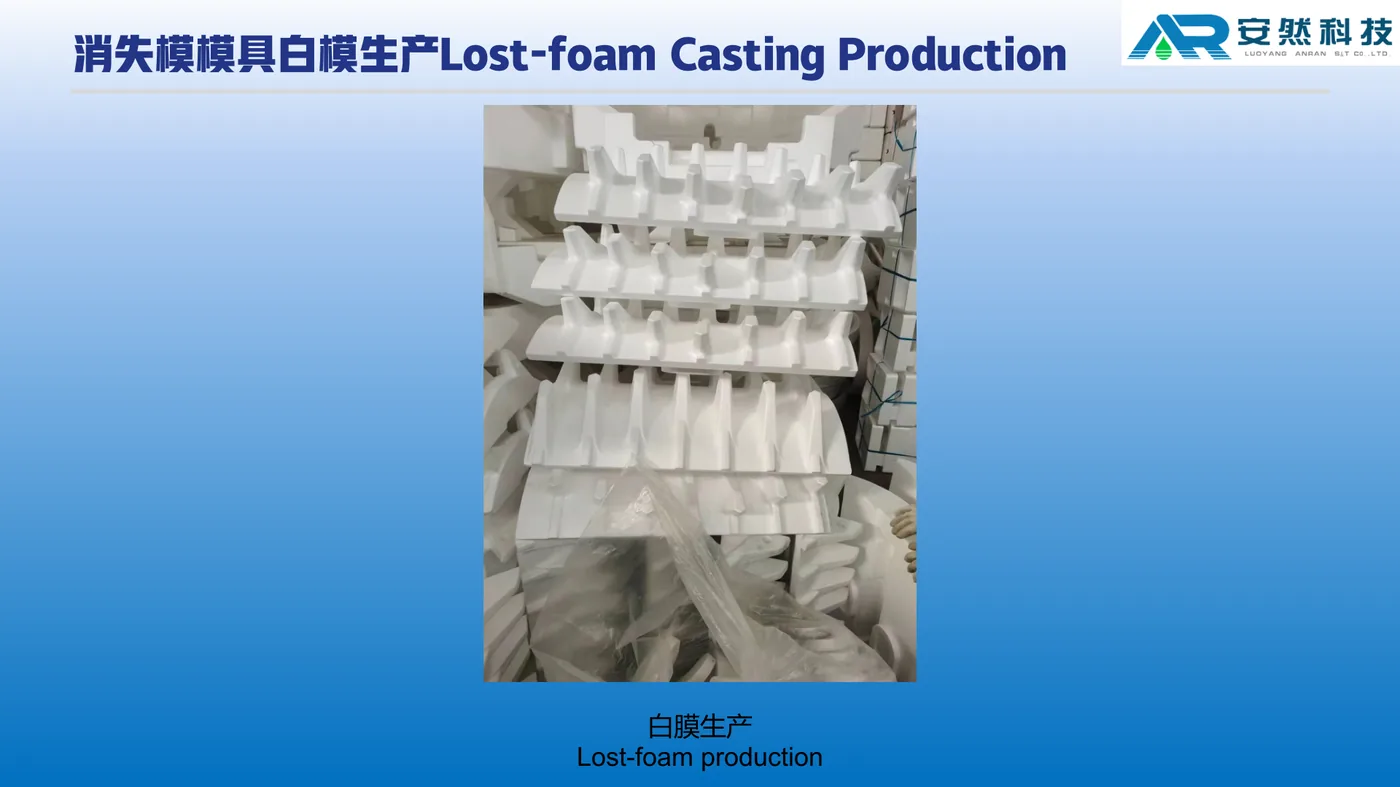
  3. Tooth plate process step 03: Lost-foam white pattern production
    03Lost-foam white pattern production白模生产
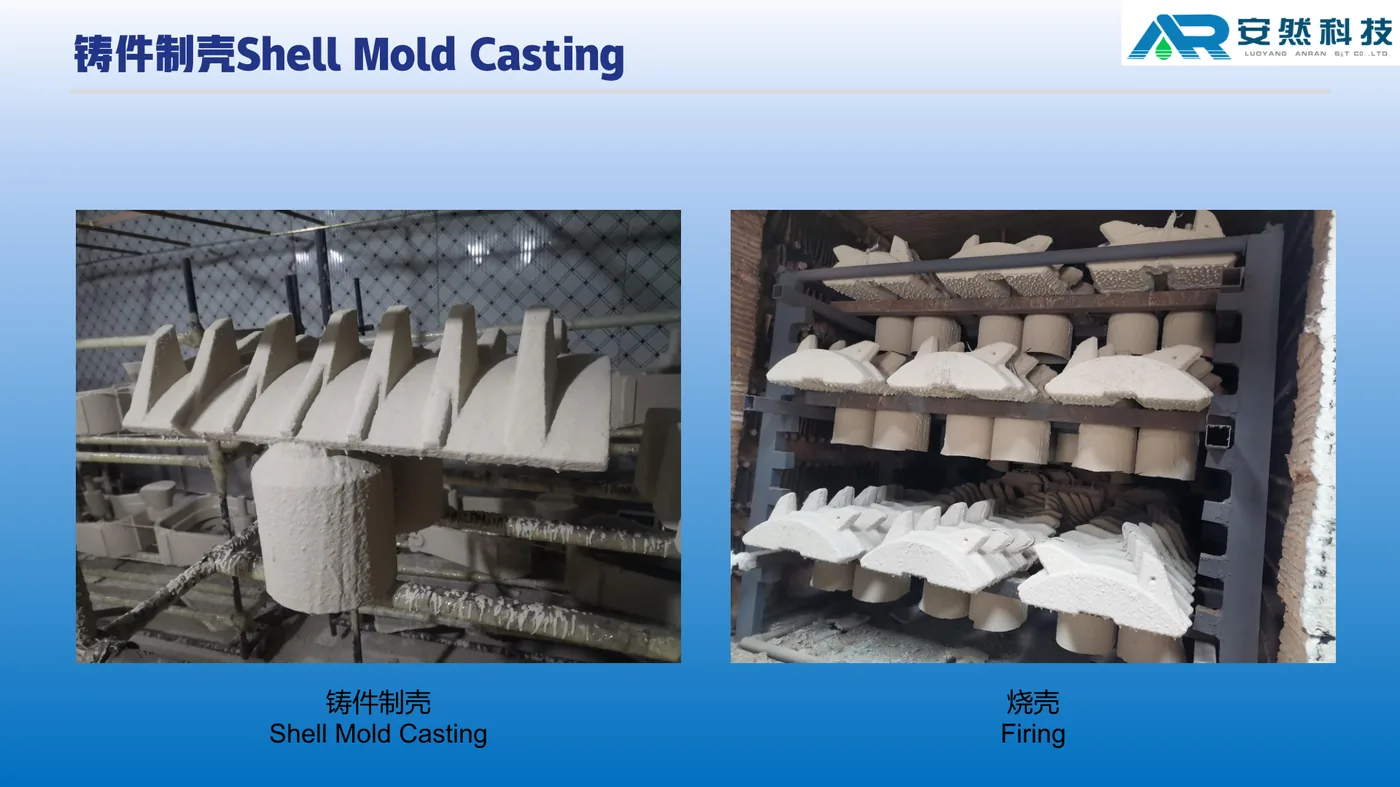
  4. Tooth plate process step 04: Shell mold casting and firing
    04Shell mold casting and firing消失模壳生产 / 制壳烧壳
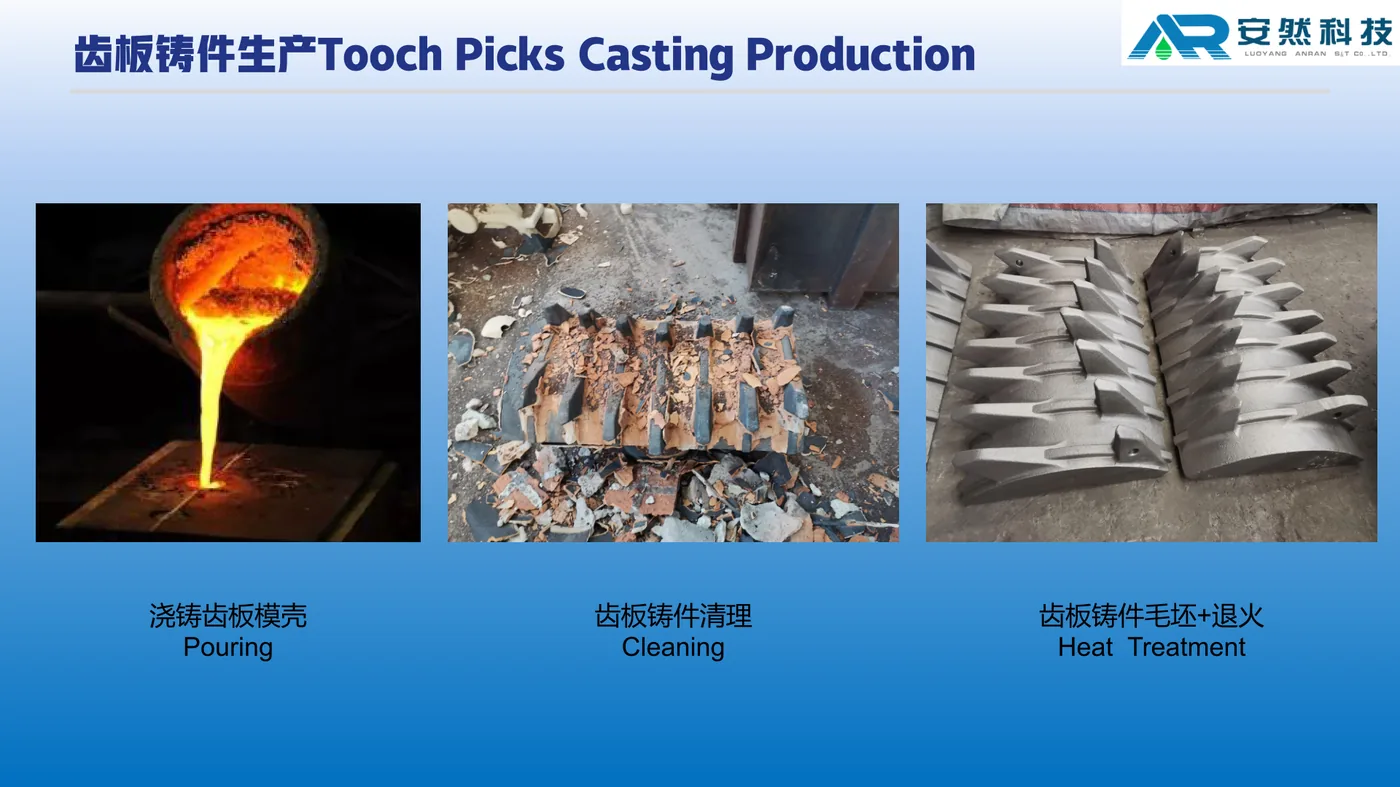
  5. Tooth plate process step 05: Tooth plate casting, cleaning and annealing
    05Tooth plate casting, cleaning and annealing齿板铸件生产 (浇铸, 清理, 毛坯+退火)
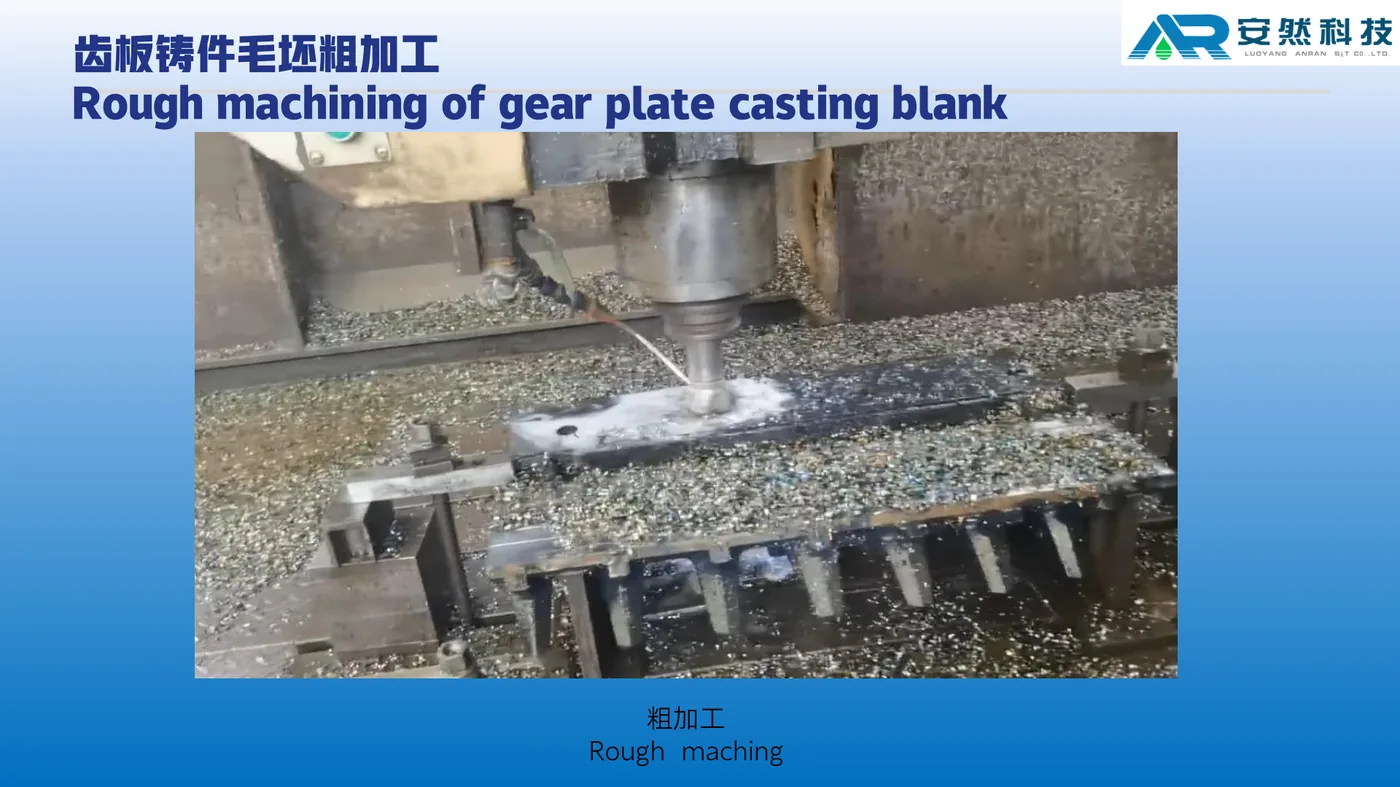
  6. Tooth plate process step 06: Rough machining
    06Rough machining铸件毛坯粗加工
  7. Tooth plate process step 07: Material-appropriate NDT and approved defect repair
    07Material-appropriate NDT and approved defect repair无损探伤 NDT 及缺陷修复
  8. Tooth plate process step 08: Heat treatment (quench and temper)
    08Heat treatment (quench and temper)热处理工艺 (淬火+回火)
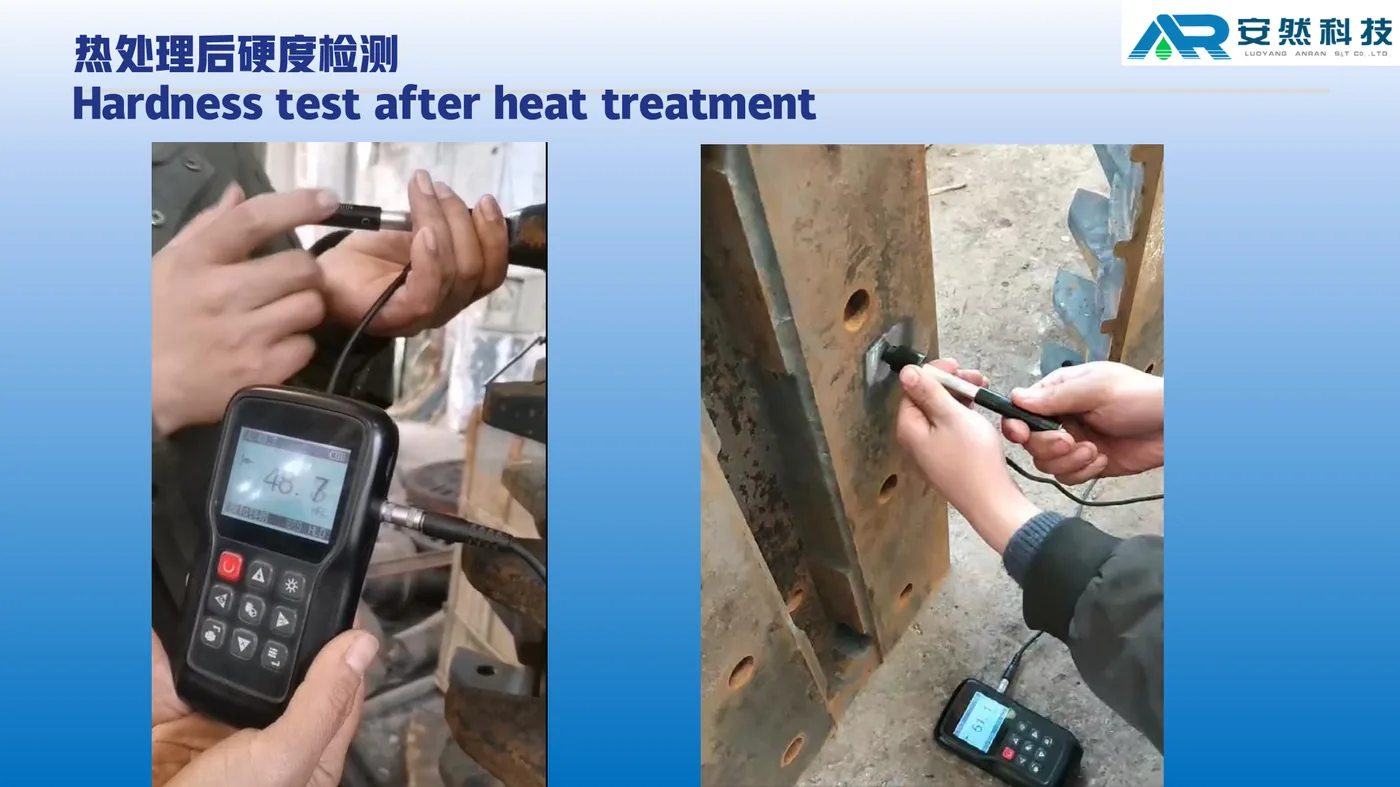
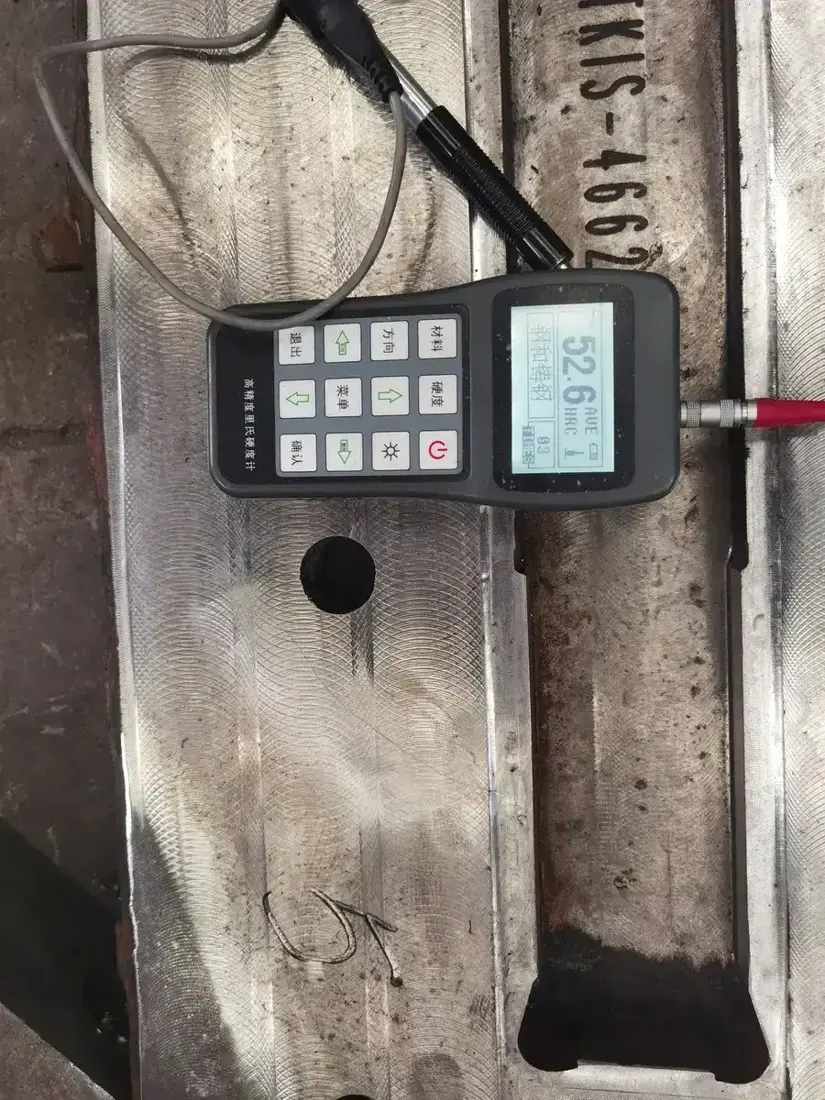
  9. Tooth plate process step 09: Hardness test after heat treatment
    09Hardness test after heat treatment热处理后硬度检测
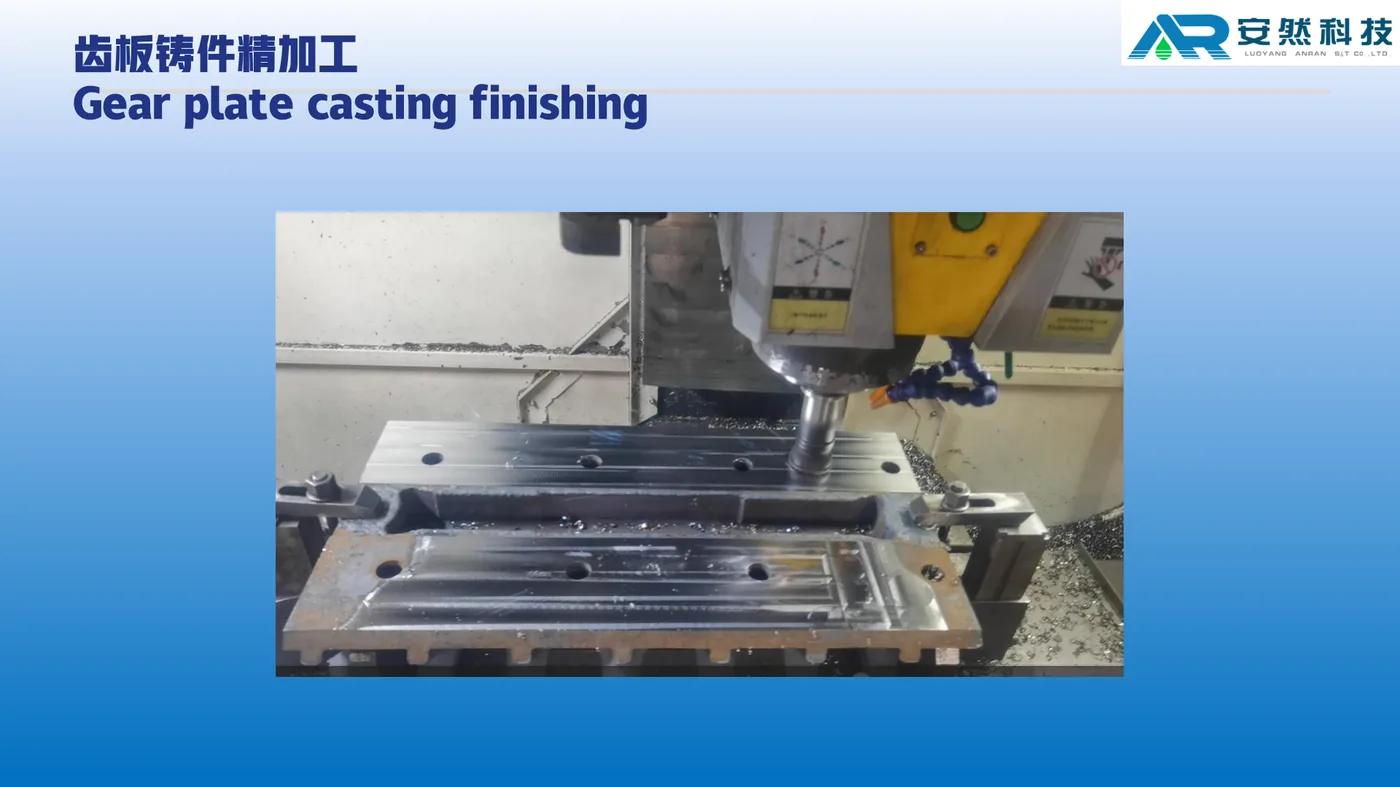
  10. Tooth plate process step 10: Finish machining
    10Finish machining齿板精加工
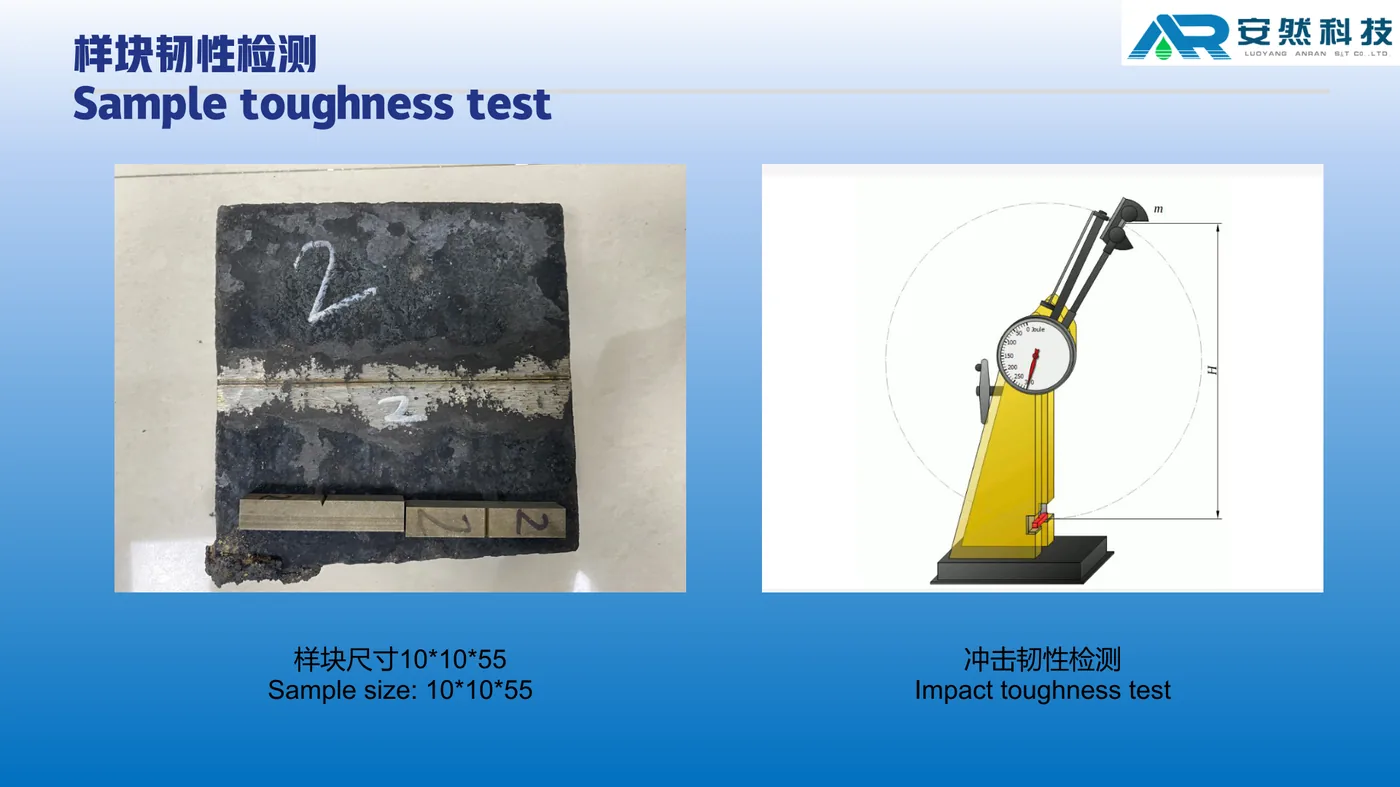
  11. Tooth plate process step 11: Sample toughness test (10×10×55 impact)
    11Sample toughness test (10×10×55 impact)样块韧性检测 (样块 10×10×55, 冲击韧性)
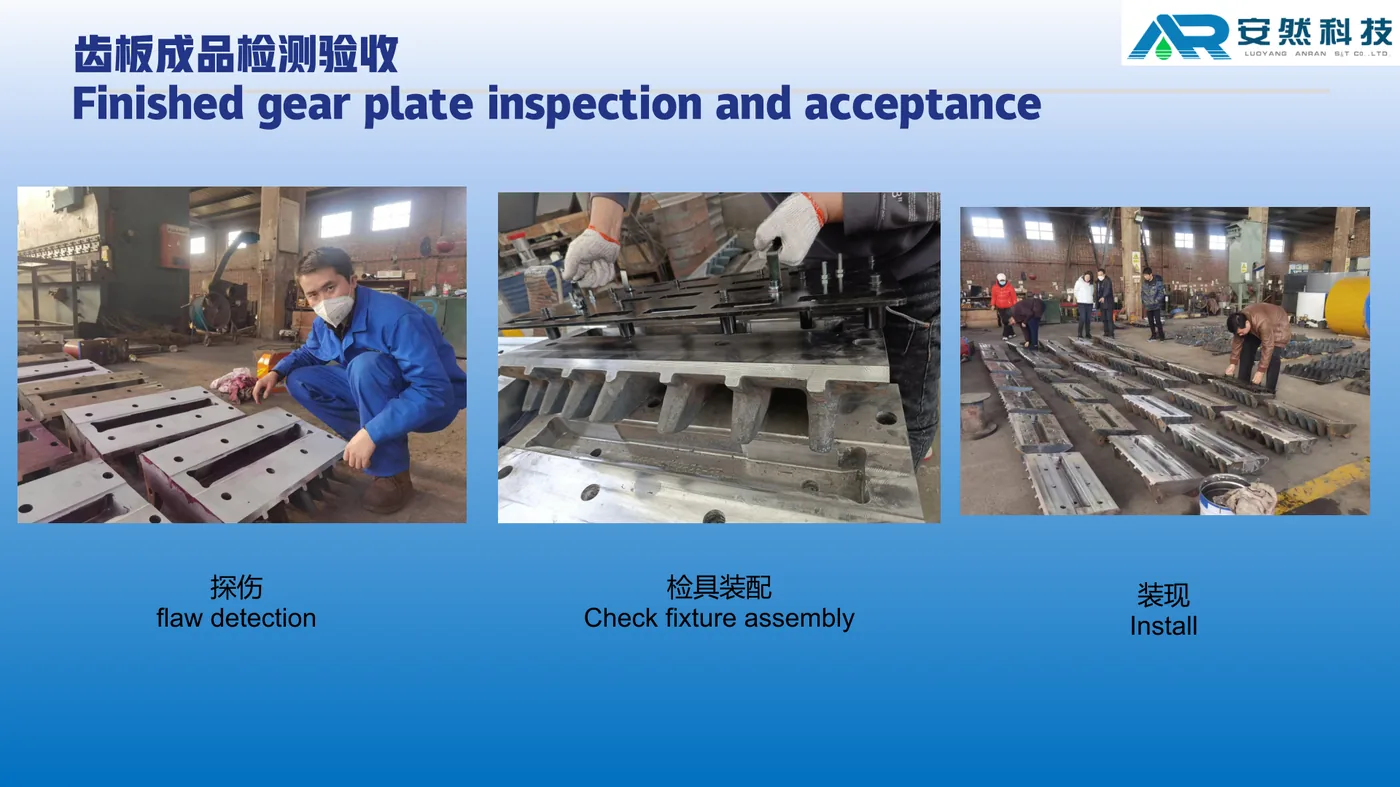
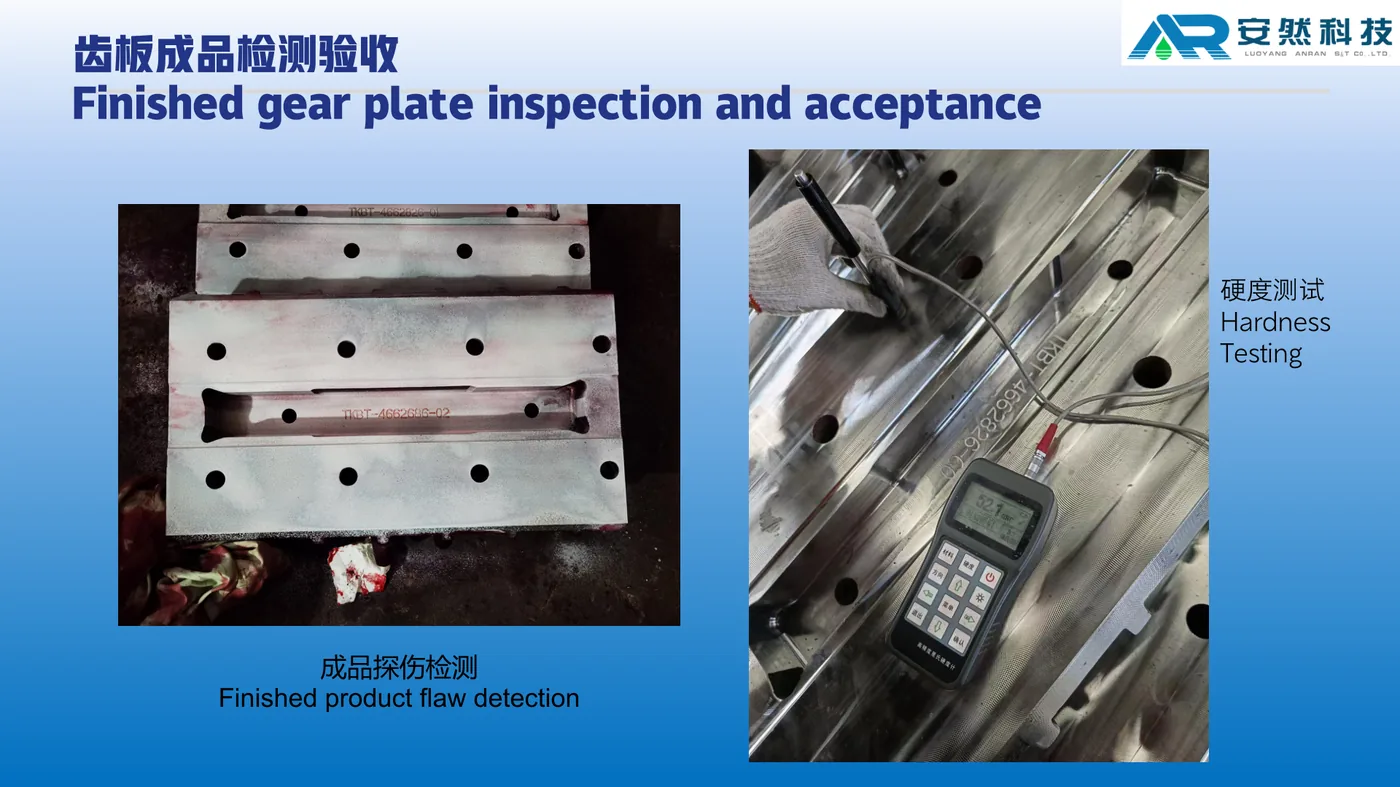
  12. Tooth plate process step 12: Finished inspection with applicable NDT, gauge fit and trial assembly
    12Finished inspection with applicable NDT, gauge fit and trial assembly齿板成品检测验收 (探伤, 检具装配, 装现)
  13. Tooth plate process step 13: Finished tooth plate
    13Finished tooth plate齿板成品

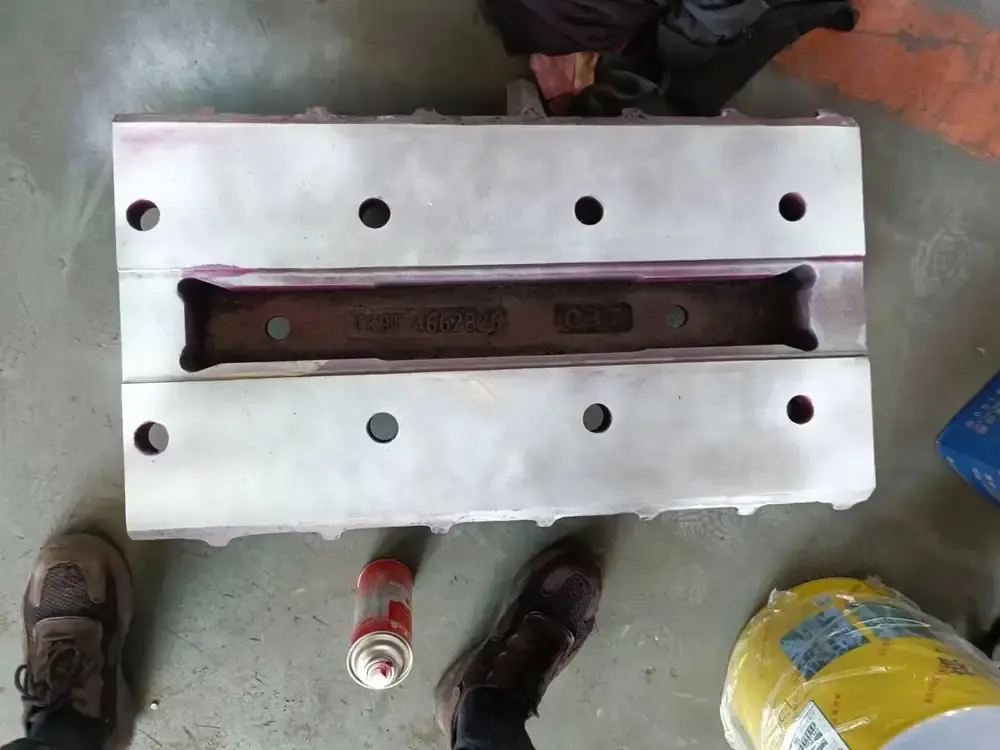
NDT methods follow material, microstructure, thickness, surface condition and discontinuity type: MT for suitable ferromagnetic materials; PT for applicable surface-breaking discontinuities; UT/RT to approved procedures, reference standards, coverage and acceptance levels. Photos below are from ANRANST tooth-plate production. Workshop hardness checks and segment machining archives can be reviewed together with heat-treatment hardness sampling and installed-base identification.

ANRANST workshop hardness check on tooth plate
Post heat-treatment hardness check (workshop archive)
ANRANST workshop tooth-segment machining
Segment / tooth-plate machining floor (workshop archive)
Standard Models and Key Dimensions

RollSizer DRS standard series and principal dimensions

The table follows the historical thyssenkrupp RollSizers brochure and DRS 1000 × 3000 C data sheet. Capacity, power, feed and weight depend on material, tooth profile, Center/Side arrangement and project configuration; the note states the historical example conditions and is not a performance guarantee.

Series / modelNominal roll spacing / common roll lengthsHistorical maximum-feed examplesCapacity / installed-power examples
DRS 500500 mm / 1000–2000 mmApprox. 480–650 mm (SideSizer approx. 200 mm)Up to approx. 1500 t/h / 55–220 kW
DRS 660660 mm / 1500–3000 mmApprox. 650–850 mm (SideSizer approx. 300 mm)Up to approx. 2500 t/h / 160–500 kW
DRS 800800 mm / 1500–3000 mmApprox. 750–1050 mmUp to approx. 3500 t/h / 200–630 kW
DRS 10001000 mm / 2000–3000 mmApprox. 950–1300 mmUp to approx. 5000 t/h / 250–700 kW
DRS 12501250 mm / 2000–3000 mmApprox. 1200–1600 mmUp to approx. 7500 t/h / 450–800 kW
DRS 15001500 mm / 3000–4000 mmApprox. 1400–2000 mmUp to approx. 10000 t/h / 750–1200 kW
DRS 1000 × 3000 C (B)1000 mm / 3000 mmFeed opening 3000 × 2280 mm (project example)Coal/lignite; up to approx. 3000 t/h; 2 × 200 or 2 × 250 kW; machine envelope 6600 × 3740 × 1625 mm

Historical brochure examples use medium-hard limestone, about 50% fines in the feed, a 5:1 reduction ratio and an example bulk density of 1.6 t/m³. Maximum feed depends on tooth configuration. Do not treat the table as a performance guarantee for other duties.

The DRS 1000×3000 C(B) row is a project data-sheet example: keep feed opening, machine envelope and capacity/power as separate fields, and do not read them as the brochure maximum-feed column used above.

Series numbers and roll length support preliminary identification only. Before manufacture confirm the full model suffix, serial number, tooth profile and rows, breaker-bar option, drive arrangement and drawing revision.

thyssenkrupp

Component Location Diagram

The numbers on the diagram correspond one to one with the rows below.

thyssenkrupp RollSizer DRS – Component Location Diagram
Pictured model: DRS CenterSizer OEM family view (dimensions not specified)
No.ComponentLocationApplies to
1Toothed rollsCentral twin-roll tooth rowsDRS CenterSizer
2Drive motorFront drive moduleDRS CenterSizer
3Gear reducerBetween the motor and roll shaftDRS CenterSizer
4CouplingMotor-to-reducer connectionDRS CenterSizer
Wear Parts

Chamber wear parts, positions and materials

Identify tooth segments, rings, breaker bars, side combs, liners and fasteners separately. Each card links to the corresponding component and material pages.

Spare Parts

Roll shafts, supports and drive spares

Drive components are separate from wear parts. Confirm shafts, bearing housings, gearboxes and synchronizing systems against installed interfaces, loads and drawings.

Crushing roll shaft assembly
01

Crushing roll shaft assembly

Crushing Roll Shaft Assembly

Includes the shaft, segment mounting zones, end connections and bearing seats. Confirm spacing, length, tooth profile, shaft position, rotation direction and complete shafting drawings.

View the common part page →
FAQ

Frequently asked questions

Is DRS 1000 enough to identify a tooth segment?

No. Confirm roll length, C/S arrangement, row count, profile, breaker bar, shaft position, serial number and drawing revision.

Do CenterSizer and SideSizer use the same wear parts?

Not entirely. CenterSizer mainly crushes between the rolls; SideSizer forms the working gap between teeth and side combs. Check segments, side liners and fixings separately.

Why link both thyssenkrupp and FLS?

This page records thyssenkrupp Mining Technologies installations from before 2022. The business joined FLS in 2022, so both legacy nameplate identity and current succession must be retained.

Can ANRANST manufacture RollSizer tooth plates / segments to this process?

Yes. ANRANST manufactures and accepts tooth plates (segments) through early proofing, metal tooling and lost-foam work, casting/cleaning/annealing, rough and finish machining, material-appropriate NDT and approved repair, heat treatment with hardness/toughness checks, and finished inspection with applicable NDT, gauge fit and trial assembly. Supply still follows the installed drawing, serial identity, duty conditions and single-point responsibility.

Submit full DRS model, nameplate, tooth sequence or worn part

Provide model suffix, serial number, Center/Side arrangement, tooth rows, breaker-bar option, drawings, photos, materials and duty. We coordinate identification, material assessment, manufacture, quality control and delivery.

Equipment Brand and ModelDrawingDrawing or DimensionsCurrent MaterialPhotographs of Failed PartsTarget Service LifeOperating Conditions
Request a Quote

Or contact us directly: +86 156 3797 3199
zzx@anranst.com

Manufacturing Services in China

From Technical Assessment to Finished-Part Delivery

ANRANST provides customers worldwide with engineering assessment, production at certified foundries to the customer technical requirements, quality control and finished-part delivery for custom wear parts and industrial spares, with scope to support other custom industrial parts.

01

Drawing and Engineering Review

We review mating surfaces and interface dimensions and assess material, heat treatment and manufacturing feasibility.

02

Material and Heat-Treatment Specification

Material grades and heat-treatment processes are specified order by order, stated in the technical agreement and tracked through production.

03

Quality Control

Drawing confirmation, material and process control, production tracking, inspection and acceptance coordination.

04

Finished-Part Delivery

We coordinate manufacturing, quality confirmation, packaging and delivery of complete finished parts in a workable, closed-loop supply process.

Provide the equipment brand, complete model and serial number, part name, part number or drawing number, drawing revision, quantity, material requirements and duty. If identifiers are unavailable, send photographs and key dimensions.

Submit an Enquiry