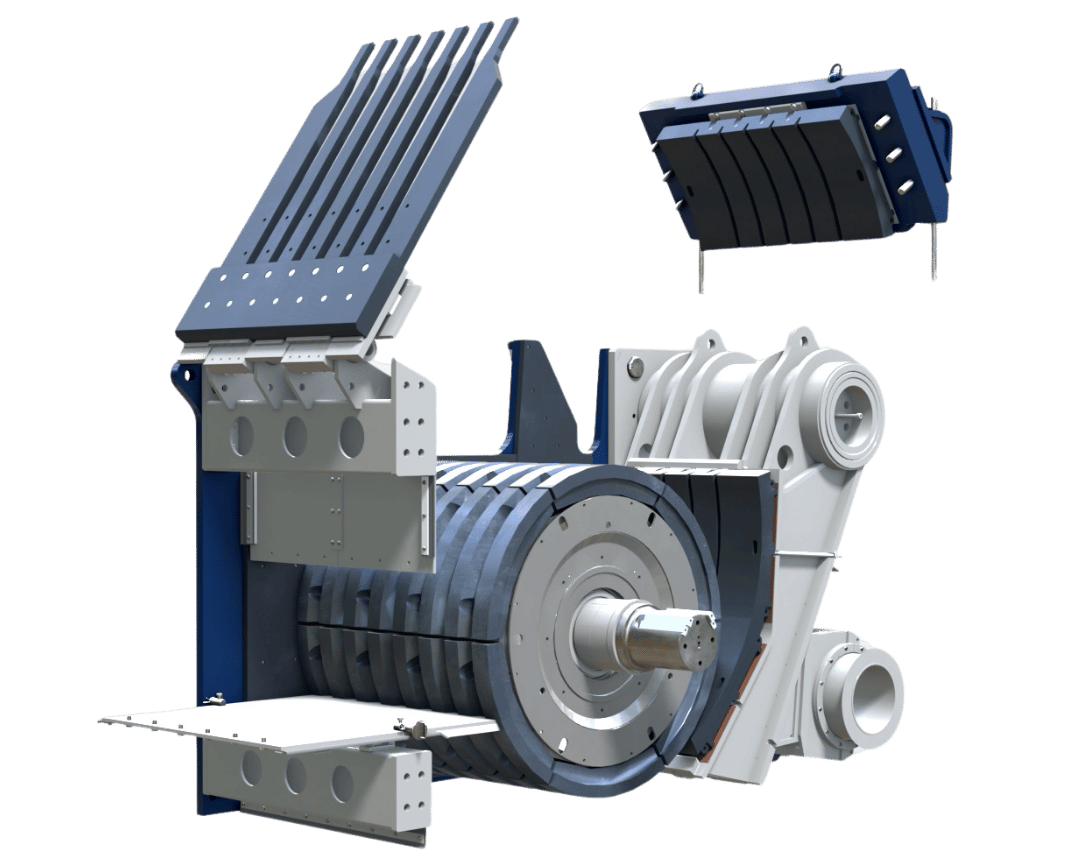
FLS الكسارات الأسطوانية اللامركزية ERC

Start with five standard models and key dimensions to identify jaw liners, roll surfaces, grates, hood wear protection, eccentric roll shafts, bearings and hydraulic spares, then confirm materials and drawing numbers for an enquiry.

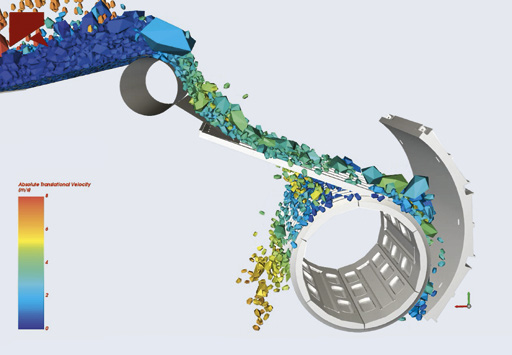
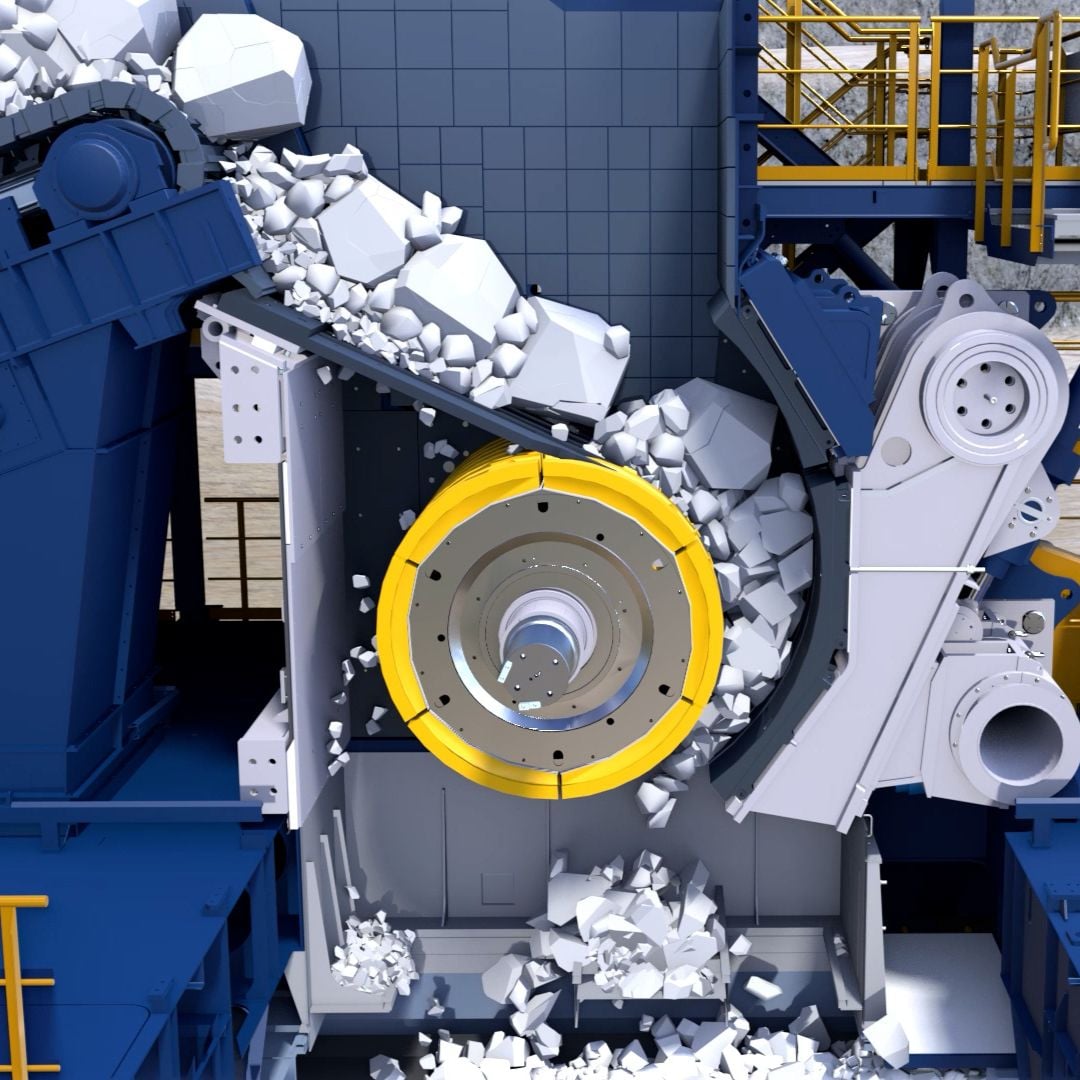
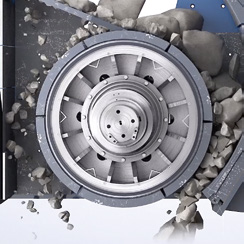
Official FLS ERC eccentric roll crusher working-area image
Official FLS ERC working-area image, showing the integrated static grate, eccentric roll, crushing jaw and lower discharge path.
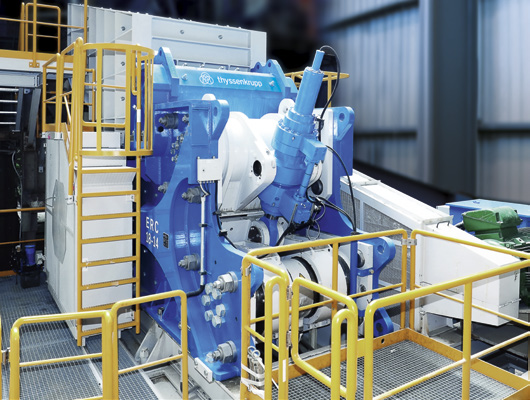
Official FLS ERC eccentric roll crusher maintenance image
Official FLS ERC maintenance image, showing the relative positions of the grate, hood, eccentric roll, crushing jaw and hydraulic adjustment structure.
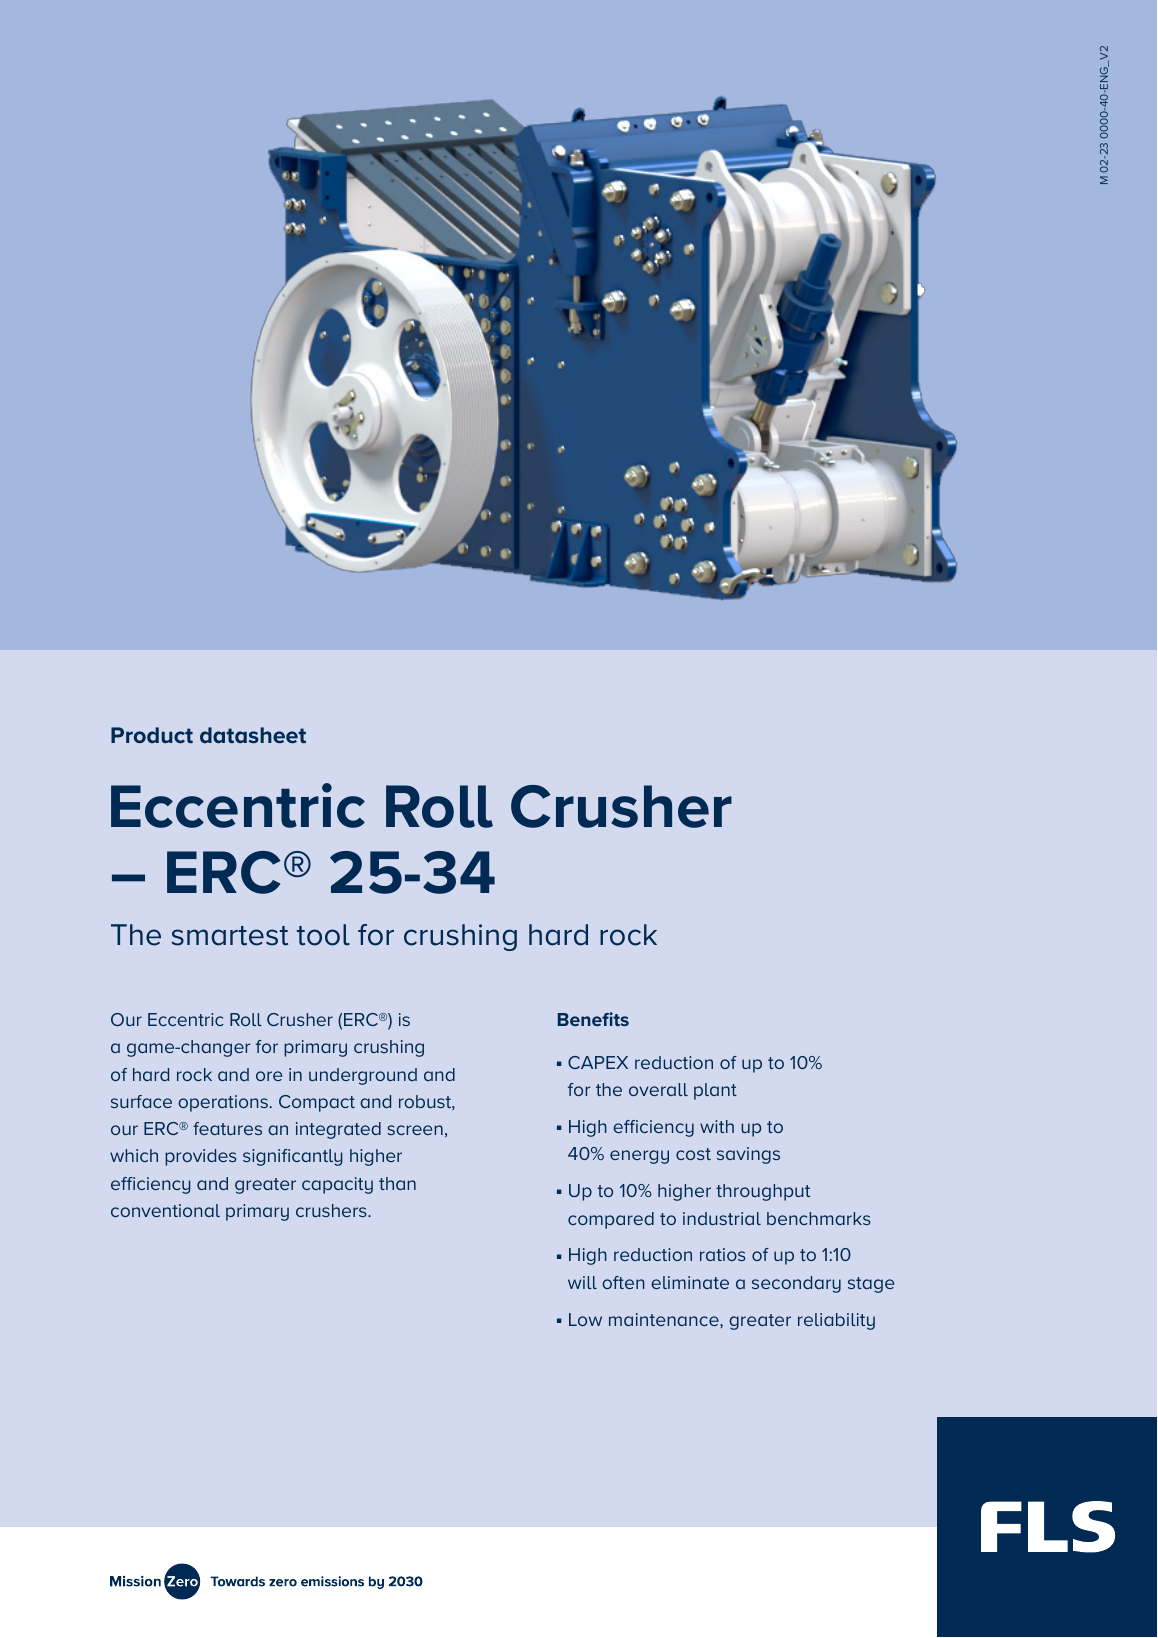
First page of the official FLS ERC 25-34 datasheet
First page of the official FLS ERC 25-34 datasheet. The model table also includes 18-14, 22-20, 25-25 and 25-30.
OEM المعدات التفاصيل

الطرازات وقطع التآكل وقطع الغيار والمواد في صفحة واحدة

ERC combines an eccentric single-roll crusher with a static grate. This page covers the standard models, dimensions, installation positions, material selection, drawing checks and enquiry information directly needed for spare identification.

5 Published standard models
7 Wear parts
3 Core spares
6 Official sources
Standard Models and Key Dimensions

ERC 18-14 to ERC 25-34

Models, capacity, feed opening, roll diameter and width, CSS, drive power, equipment weight and overall dimensions come from the corresponding official FLS datasheets.

ModelCapacityFeed openingRoll diameter / widthCSS rangeDrive powerالمعدات weightOverall dimensions L×W×H
ERC 18-14550–1,850 t/h1,400 × 1,000 mm1,800 / 1,400 mm70–220 mm160–300 kWApproximately 83,000 kgApproximately 5,200 × 3,250 × 3,200 mm
ERC 22-201,050–3,450 t/h2,000 × 1,200 mm2,200 / 2,000 mm80–260 mm300–450 kWApproximately 156,000 kgApproximately 6,200 × 4,250 × 3,800 mm
ERC 25-251,450–4,900 t/h2,500 × 1,300 mm2,500 / 2,500 mm100–260 mm450–600 kWApproximately 185,000 kgApproximately 7,100 × 4,700 × 4,300 mm
ERC 25-302,150–7,300 t/h3,000 × 1,300 mm2,500 / 3,000 mm100–300 mm500–700 kWApproximately 215,000 kgApproximately 7,100 × 5,200 × 4,300 mm
ERC 25-342,600–8,800 t/h3,400 × 1,300 mm2,500 / 3,400 mm100–300 mm600–800 kWApproximately 240,000 kgApproximately 7,100 × 5,600 × 4,300 mm

تعتمد السعة على الكثافة الظاهرية ومقاومة الانضغاط وتوزيع الأحجام والرطوبة وحجم المنتج المستهدف وإعداد الجانب المغلق (CSS) الفعلي. أكِّد قطع الغيار النهائية وفقًا للطراز الكامل والرقم التسلسلي ورقم الرسم ومراجعة الرسم وأبعاد التركيب.

قطع الغيار المستهلكة

Crushing jaw, eccentric roll, grate, hood and discharge protection

Parts are ordered by actual installation position: jaw liners and roll surfaces in the chamber first, followed by static grates, side guards, hoods and discharge areas. Each item links to its part and material pages.

Crushing jaw liner position reference in the FLS ERC
01

Crushing Jaw Liners

Crushing Jaw Liner

Attached to the swing jaw, these form the fixed wear face on the jaw side of the ERC chamber. Check model, liner segments, tooth profile, thickness, hole pattern, assembly direction, CSS range and used-part wear profile.

Material and manufacturing checks:Use high-manganese steel, wear-resistant alloy steel or application-validated composite wear solutions. Confirm grade, heat treatment and hardness against original drawings, ore impact conditions and wear records.

View Part التفاصيل →
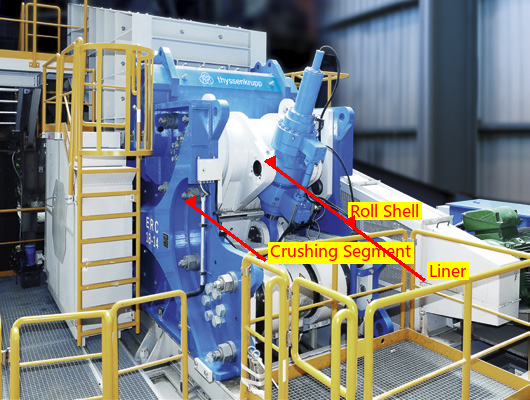
Eccentric roll liner and surface positions in the FLS ERC
02

Eccentric Roll Liners / Roll Surfaces

Roll Liner / Roll Surface

These fit around the eccentric roll and form the principal wear surface working against the jaw liners. Check roll diameter and width, segment count, circumferential location, fastenings, surface profile and rotation direction.

Material and manufacturing checks:Select wear-resistant alloy steel, high-manganese steel or composite wear protection according to the balance of impact, compression and abrasion. Outside diameter alone is insufficient for replacement selection.

View Part التفاصيل →
Segmented roll liner positions in the FLS ERC
03

Segmented Roll Liners

جزء غلاف البكرة

For segmented roll surfaces, identify each segment by circumferential position and assembly sequence. Check arc length, width, interfaces, fastening holes, locating structure and adjacent segment overlaps.

Material and manufacturing checks:Even when the material matches the complete roll surface, separately check casting batch, heat treatment, dimensional deviations, weight differences and assembly clearances.

View Part التفاصيل →
Integrated static grate wear part positions in the FLS ERC
04

Integrated Static Grate قطع الغيار المستهلكة

Integrated Static Grizzly قطع الغيار المستهلكة

The integrated static grate on the feed side allows fines to bypass the crushing chamber. Check grate length, openings, bar cross-section, spacing, support positions, wear direction and replacement access.

Material and manufacturing checks:Confirm wear-resistant alloy steel or quenched and tempered wear plate according to large-rock impact, abrasion, section thickness and welded/mechanical fastening method.

View Part التفاصيل →
Side guard and chamber liner positions in the FLS ERC
05

Side Guards / Chamber Liners

Side Liner / Cheek Plate

These protect chamber sidewalls and areas near the roll ends. Check left/right side, plate shape, thickness, hole pattern, jaw and roll clearances, discharge passages and wear zones.

Material and manufacturing checks:Confirm quenched and tempered wear plate, wear-resistant cast steel or bimetallic composite plate according to the balance of impact and sliding wear.

View Part التفاصيل →
Hood liner positions in the FLS ERC
06

Hood Liners

Hood Liner

FLS datasheets identify the lined hood as one of the largest components handled during routine maintenance. Check machine model, hood profile, liner segmentation, lifting points, fastening holes and maintenance opening direction.

Material and manufacturing checks:Confirm quenched and tempered wear plate or wear-resistant cast steel according to thickness, impact, replaceability and lifting weight.

View Part التفاصيل →
Discharge chute liner positions in the FLS ERC
07

بطانات قناة التفريغ

بطانة قناة التفريغ

Located below the chamber, these face high-velocity material flow and localized impact. Check discharge direction, plate thickness, segment numbers, hole patterns, overlaps and blockage clearance.

Material and manufacturing checks:Confirm quenched and tempered wear plate, bimetallic composite plate or rubber composite liners according to drop height, particle size, impact and noise requirements.

View Part التفاصيل →
قطع الغيار

Eccentric roll shafts, bearing supports and hydraulic adjustment

These three core spare categories link to their general part pages. Parts with the same name are not interchangeable by appearance across ERC models. Check structure, dimensions, loads, fits, materials and drawing numbers.

Eccentric shaft and roll assembly positions in the FLS ERC
01

Eccentric Roll Shaft and Roll Body Assemblies

Eccentric Roll Shaft and Roll Assembly

FLS datasheets identify the roll assembly with bearings and liners as the largest transport unit. Check eccentricity, journals, roll diameter and width, bearing housing spacing, keys/locking assemblies, rotation direction and dynamic balance.

Material and manufacturing checks:Confirm forged transmission alloy steel, roll body structure and surface treatment against original drawings. Include ultrasonic testing, dimensional relationships and journal accuracy in inspection.

View Part التفاصيل →
Bearing, bushing and housing positions in the FLS ERC
02

Bearings, bushings and housings

Bearings, Bushings and Housings

Bearings support the eccentric roll under cyclic crushing loads. Check bearing model, clearance, journals, housing bores, locating/floating end, seals, lubrication and temperature monitoring interfaces.

Material and manufacturing checks:Confirm bearings, copper alloy bushings, steel housings and seal materials separately according to load, speed, temperature rise and lubrication conditions.

View Part التفاصيل →
Hydraulic gap adjustment and tramp release system in the FLS ERC
03

Hydraulic Gap Adjustment and Tramp Release Systems

Hydraulic Gap Setting and Tramp Release System

These adjust CSS, compensate for liner wear and release uncrushable objects. Check cylinder bore, stroke, working pressure, mounting trunnions, valve blocks, accumulators, ports and seal grooves.

فحوصات المادة والتصنيع: أكِّد فولاذ الأسطوانة الهيدروليكية السبائكي والمعالجة السطحية وأختام NBR أو HNBR أو FKM أو البولي يوريثان وفقًا للضغط والسائل ودرجة الحرارة.

View Part التفاصيل →
Drawing and spare part numbers

طابق أرقام الشركة المصنعة الأصلية أو الأرقام الخارجية مع الطراز والموضع والأبعاد الحرجة

When submitting a number, include the full ERC model, serial number, part name, installation position, general arrangement or assembly drawing, used-part photos, critical dimensions, material and operating conditions.

Which standard FLS ERC models are publicly listed?

Current official documents list ERC 18-14, 22-20, 25-25, 25-30 and 25-34.

Is the equipment model alone enough to manufacture liners?

No. Also check the serial number, OEM drawing number, drawing revision, installation position, roll diameter and width, segmentation, fastening structure, material and used-part wear records.

Submit FLS ERC models, drawing numbers, liners or core spare requirements

Provide the full model, serial number, OEM/third-party number, drawings, used-part photos, critical dimensions, material and operating conditions. We use these to identify parts, assess materials, match manufacturing requirements, control quality and deliver finished components.

طلب مراجعة المشروع

رقم الهاتف: +86 156 3797 3199
zzx@anranst.com

خدمات صنع في الصين

من التقييم الفني إلى تسليم المنتج بالكامل

توفر شركة ANRANST للعملاء العالميين تقييمات هندسية، واختيار التصنيع الصيني، ومراقبة الجودة، وتسليم الأجزاء النهائية لقطع الغيار الصناعية المقاومة للتآكل حسب الطلب، ويمكنها أيضًا دعم قطع الغيار الصناعية الأخرى حسب الطلب.

01

مراجعة الرسومات والهندسة

قم بمراجعة أسطح التزاوج وأبعاد الواجهة، وقم بتقييم جدوى المواد والمعالجة الحرارية والتصنيع.

02

تحديد المادة والمعالجة الحرارية

تُحدَّد درجات المواد وعمليات المعالجة الحرارية لكل طلب على حدة، وتُثبَّت في الاتفاقية الفنية وتُتابَع أثناء الإنتاج.

03

ضبط الجودة

يشمل ذلك تأكيد الرسم، ومراقبة المواد والعمليات، وتتبع الإنتاج، وتنسيق عمليات الفحص والقبول.

04

تسليم المنتج النهائي

تنظيم عمليات التصنيع والتحقق من الجودة والتعبئة والتغليف وتسليم المنتجات النهائية الكاملة لتشكيل حلقة إمداد قابلة للتنفيذ.

قم بتزويدنا بالنماذج الحالية، والرسومات، وأرقام الرسومات، وأرقام الأجزاء، والمواد، أو معلومات ظروف التشغيل، وسنقوم بتحديد التحقق الفني ومسار التوريد وفقًا لذلك.

إرسال طلب