
Pins, bolts & special fasteners
للخدمة الشاقة دبابيس و خاصة المثبتات
Clamping, location, articulation and controlled assembly and removal
Pins, liner bolts, locknuts and clamping wedges in mining equipment are not ordinary hardware. They serve impact, fatigue, preload, location, sealing or sacrificial protection functions and must be confirmed against the equipment model, joint design and installation method.
Pivot pins Hammer shafts, apron pivot pins, chain pins and adjacent bushings
Special bolts Fasteners for rotating liners, wear plates, buckets and conveyor flights
Locking and location Head nuts, locknuts, washers, wedges and clamping parts
متطلبات التحديد وظيفة, preload, loads, fits, material, surface condition, assembly and removal
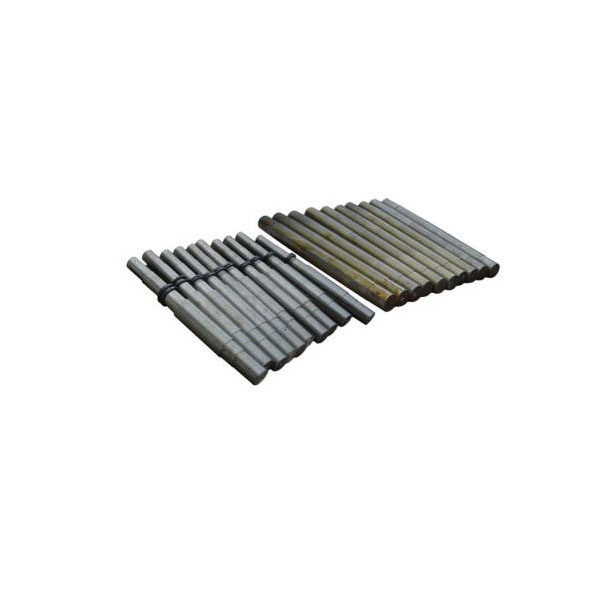
System scope
Connection identification Clamping, shear, location, articulation, rotational fatigue or sacrificial protection
Interfaces Threads, grip length, shaft diameter, holes, bushings, head, seating face and keys
Installation interfaces Torque, tensioning, elongation, lubrication, heating, hydraulics or dedicated tooling
Supply identification OEM, complete model, assembly number, part number, material and batch
Equal dimensions do not establish the same joint function
Bolted joints rely on controlled preload to maintain clamping. Pin joints transfer bearing pressure and oscillation through the pin-bushing contact. Locknuts and wedges locate liners or assemblies. Higher material strength does not automatically make a joint more reliable.
For continuous drive relationships between chain pins and bushings, see chains and sprockets; for pin bushing materials and lubrication, see bearings and bushings.
Heavy-duty pins and pivot components
Pins, bushings, housing bores and lubrication form one contact system
Surface hardness, core toughness, fits and lubrication must suit impact and oscillating conditions.
Hammer crusher hammer shafts
Locate hammers under repeated impact, shear and oscillating wear. Check the rotor, hammer bores, spacers, shaft diameter, retention and assembly/removal direction.
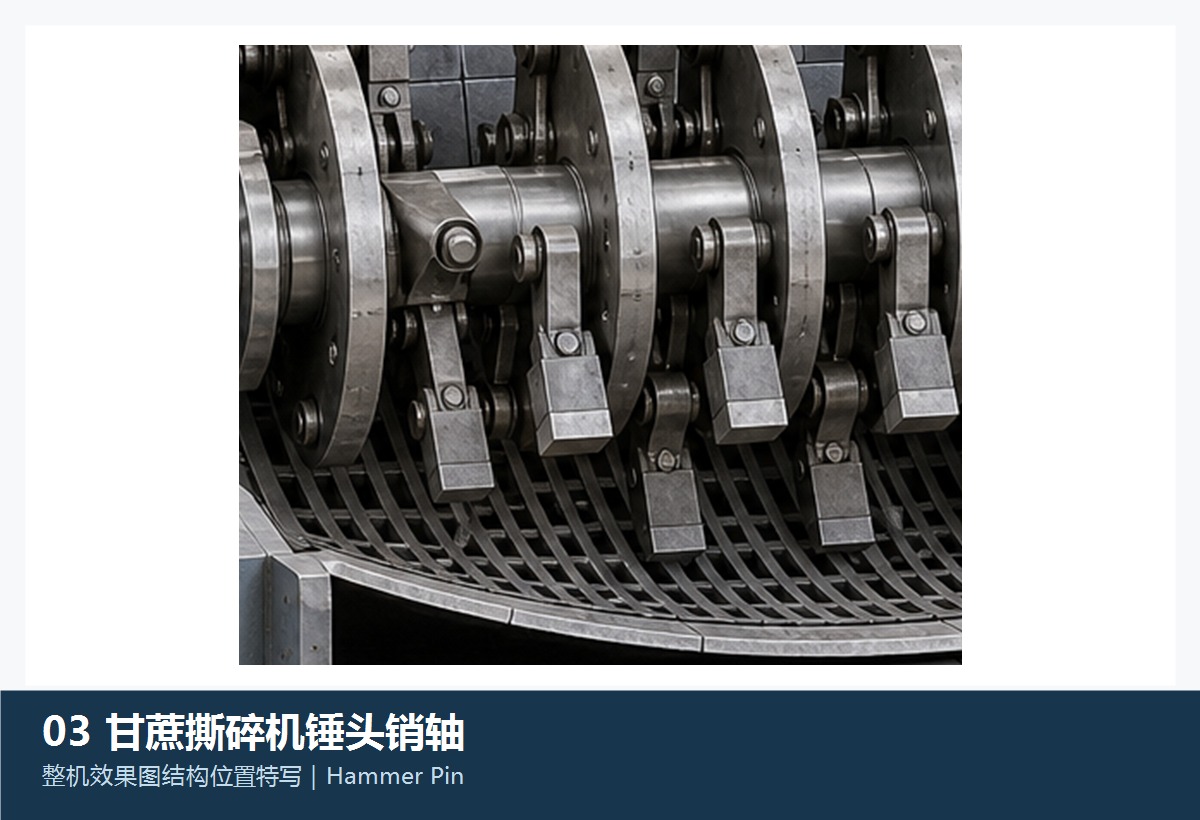
Sugarcane shredder hammer pins
Withstand high-speed swinging-hammer impact and fibre contamination. Check rotor discs, hammers, pin diameter, axial retention, wear and the wet, corrosive environment.
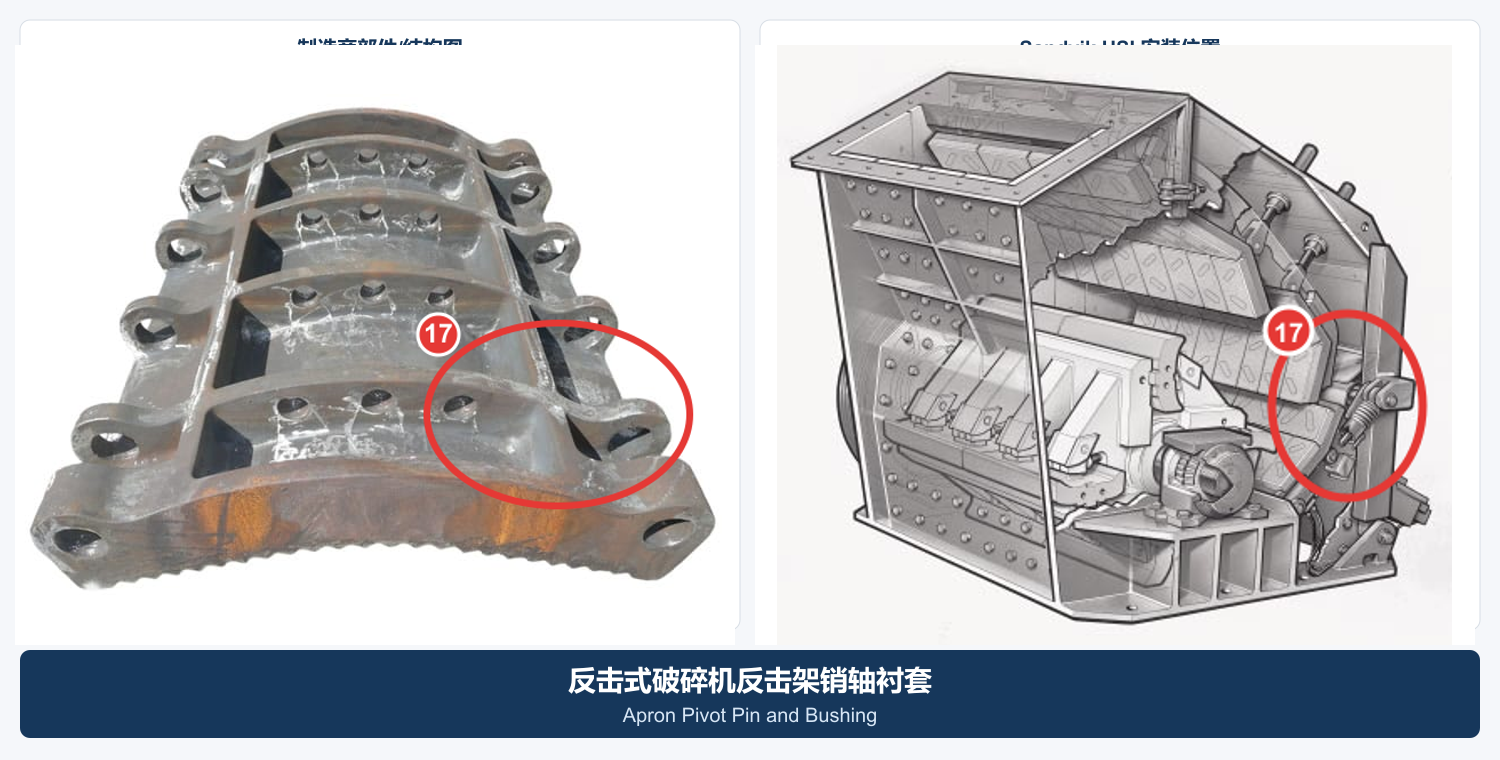
Apron pivot pins and bushings
Provide the pivot for apron movement and release. Check bearing pressure, impact, oscillation angle, lubrication, housing bore, axial location and adjacent hydraulic system.
المعدات-specific bolts and connectors
Preload, friction and grip length determine joint stability
Rotating liner bolts, structural bolts and welded studs have different load paths and installation methods.
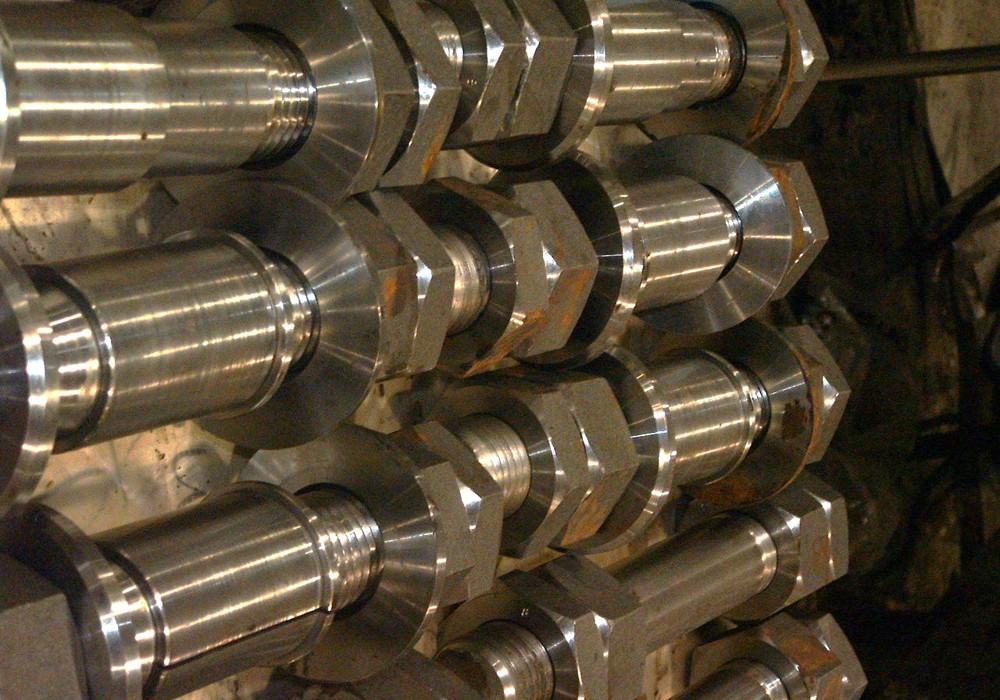
Large mill rotating-body and liner fasteners
Cover shell and head flanges, rotating-body connections and liner fastening positions. Check static structural bolts, fatigue-loaded rotating bolts, liner bolts, nuts, washers, spacers, lubrication and preload methods separately. The image represents the fastener category; confirm exact shapes against installed drawing references.
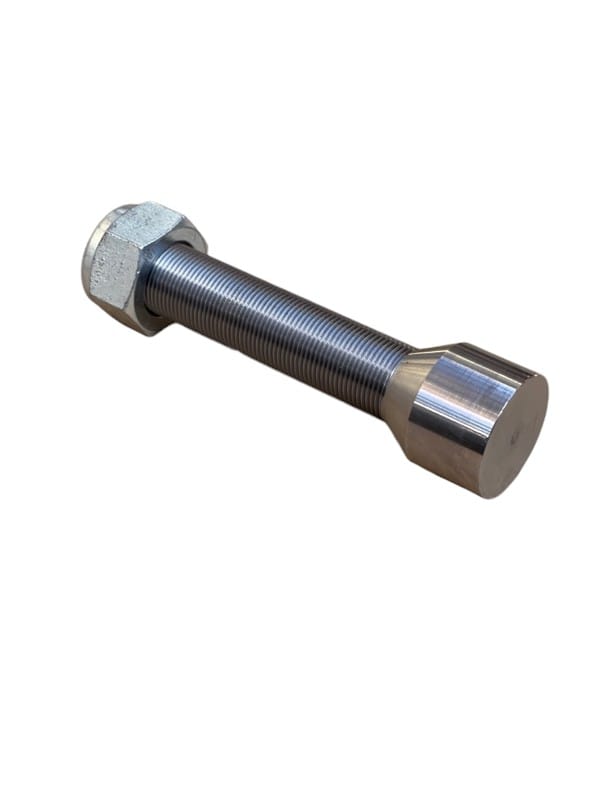
Hammer crusher liner bolts
Clamp casing liners under impact and vibration. Check head form, holes, grip length, washers or seals, preload and locking.
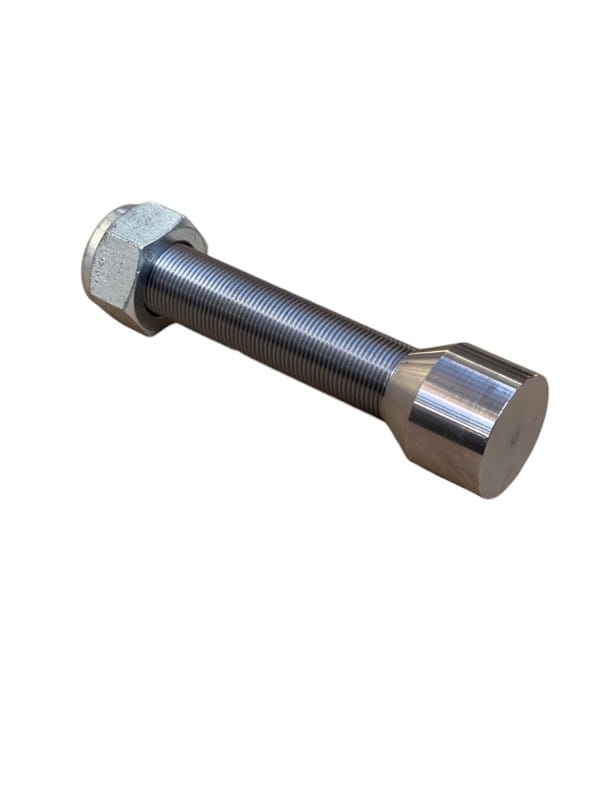
Impact crusher liner bolts
Secure wear components in the casing and impact zones. Check liner counterbores, head protection, preload, wear exposure, removal space and spare kits.
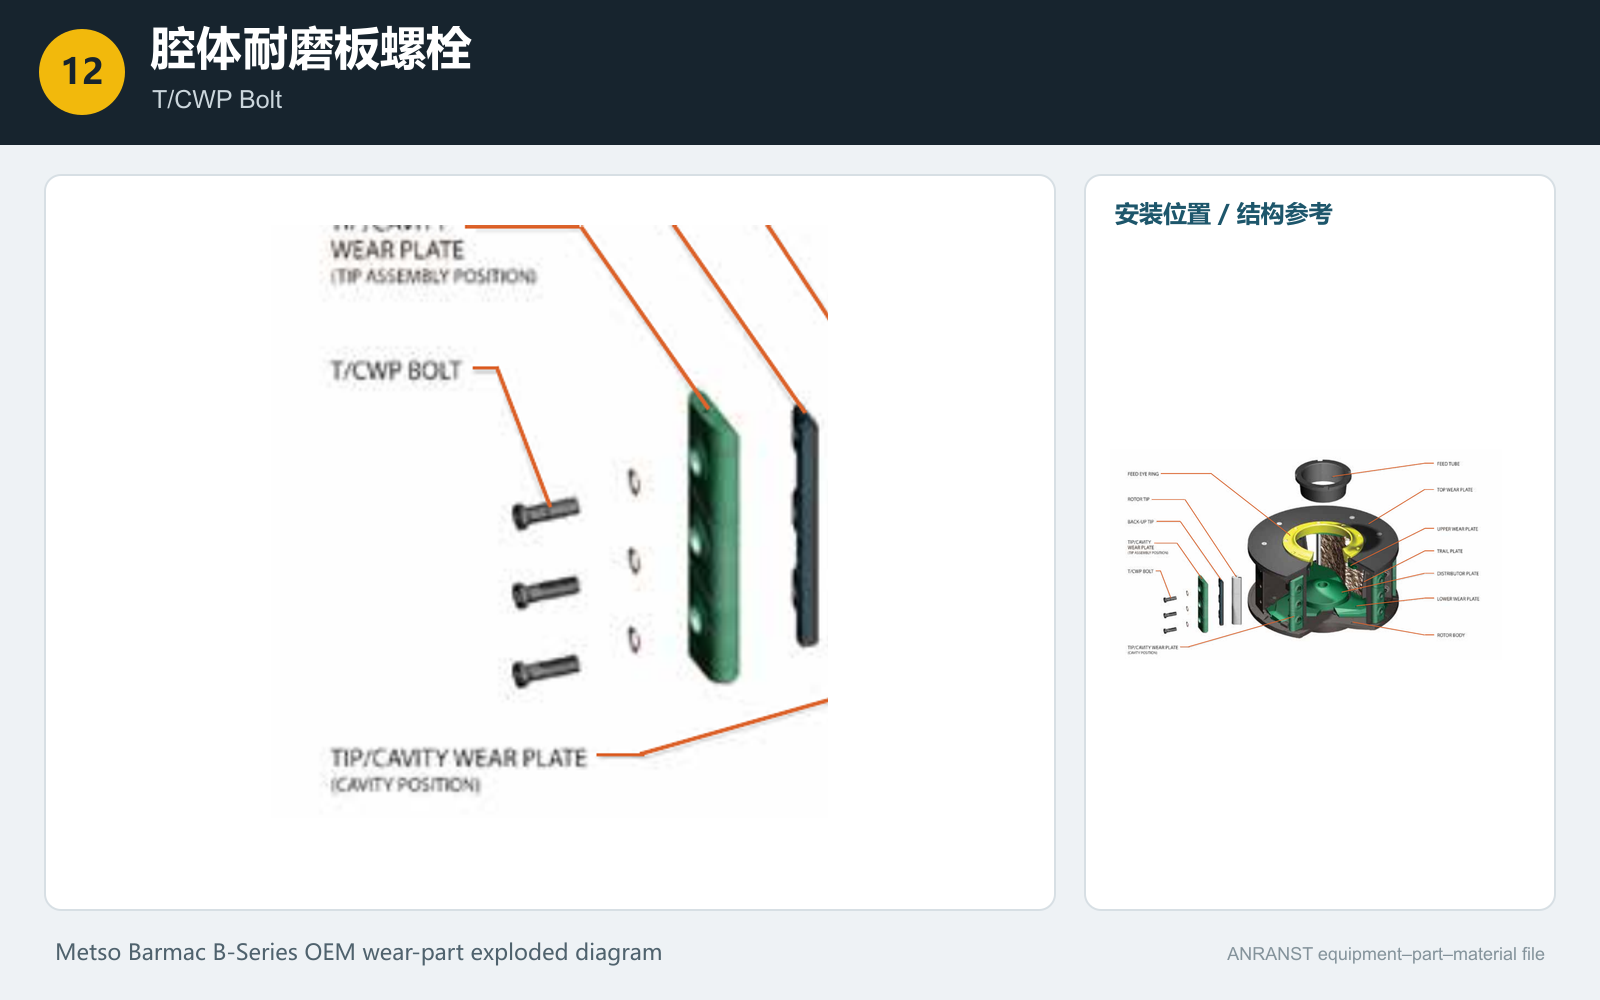
VSI Cavity Wear Plate Bolt
Clamp specific rotor or chamber wear parts. Check bolt head form, holes, rotational balance, locking method and OEM part number.
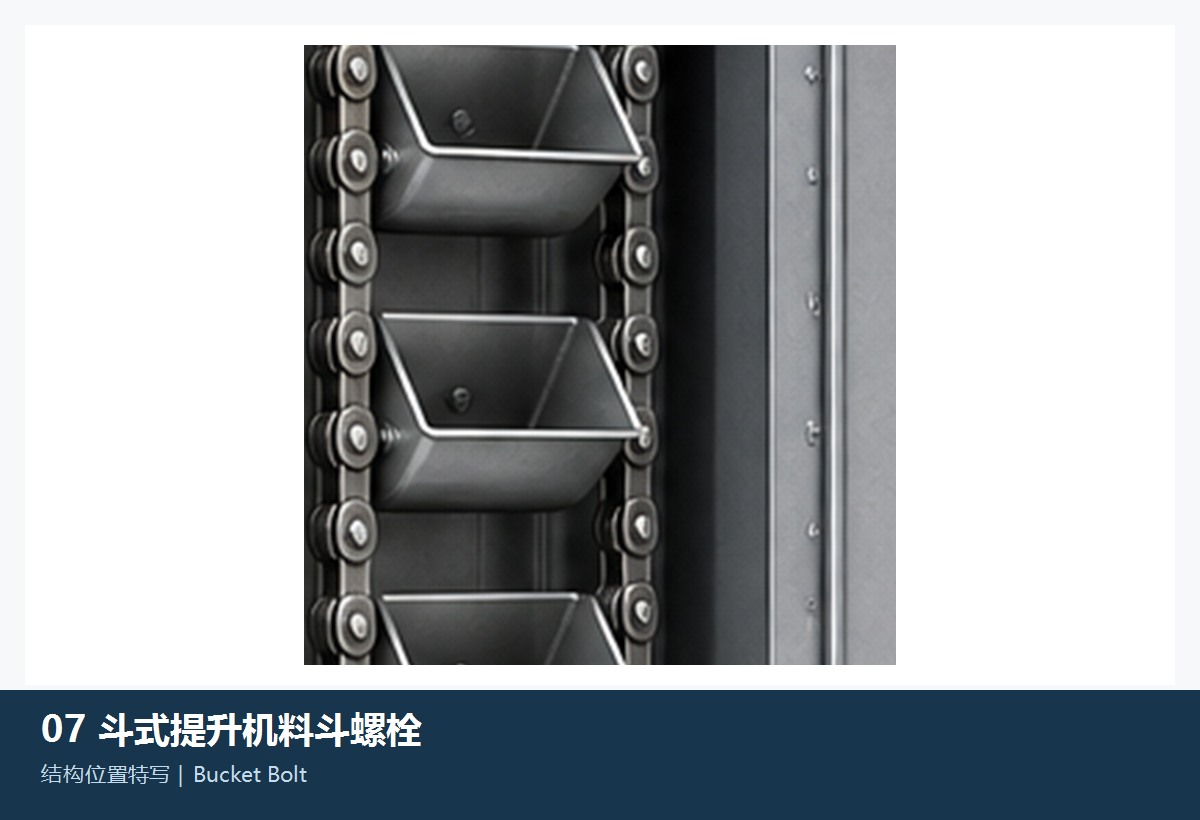
Bucket elevator bucket bolts
Secure buckets to belts or chains. Check head form, bucket holes, belt clamping, threads, vibration, material handled and locking.
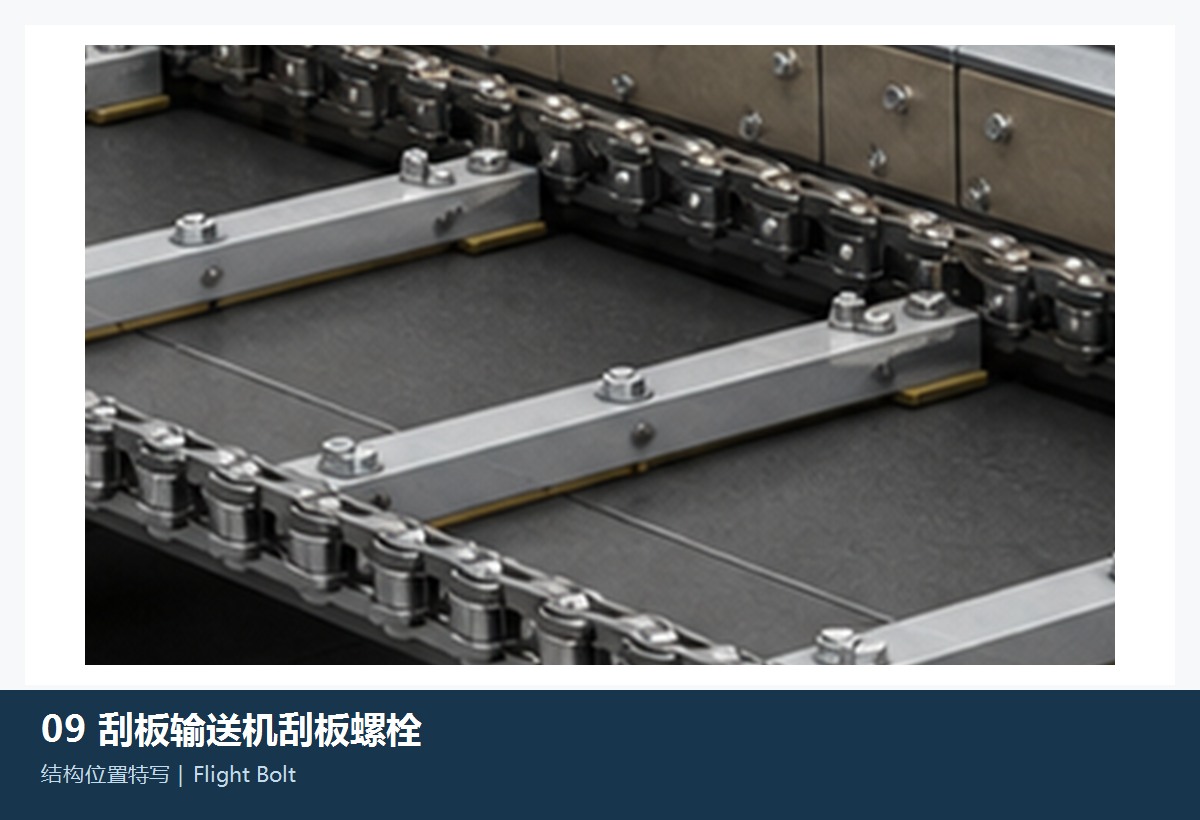
Drag conveyor flight bolts
Connect flights to chain attachments. Check chain specification, flight hole spacing, countersunk or anti-rotation features, impact and abrasion.
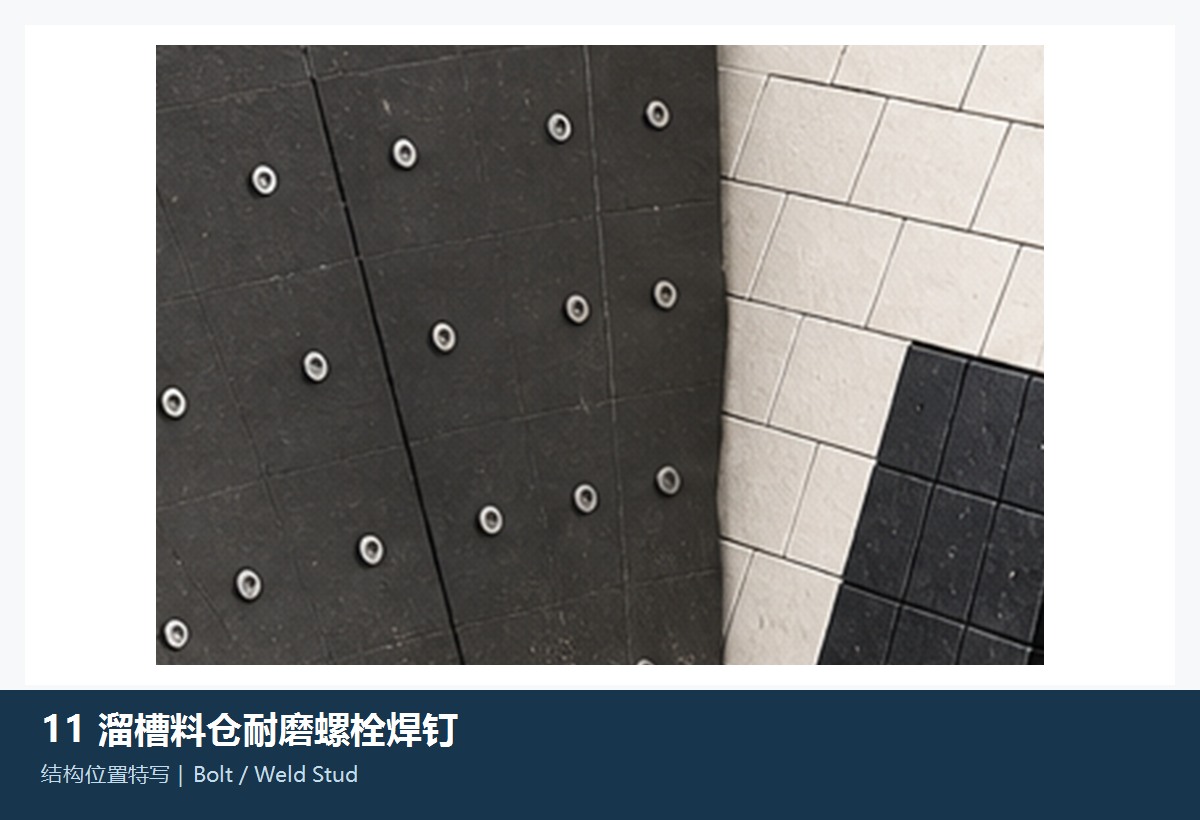
Chute liner bolts and welded studs
Secure replaceable liners or composite wear plates. Check base plate, welding procedure, hole form, wear protection, rear access and replacement method.
Locknuts, washers and clamping components
Maintain location while allowing controlled assembly and removal
Locking parts are often specific to liners, main shafts or adjustment systems and must be selected with the assembly.
Gyratory crusher head nuts
Clamp the crushing-head liner system and maintain assembly preload. Check main shaft threads, thread hand, contact faces, locking method and removal tooling.
Gyratory crusher step washers
Fit specific axial support or locking interfaces. Check installation position, steps, thickness, inside and outside diameters, loaded faces and machine version.
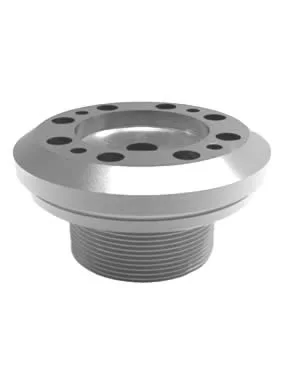
Cone crusher locknuts
Lock the crushing head or liner-related assembly. Check model, threads, thread hand, mating parts, preload, assembly/removal method and protection.
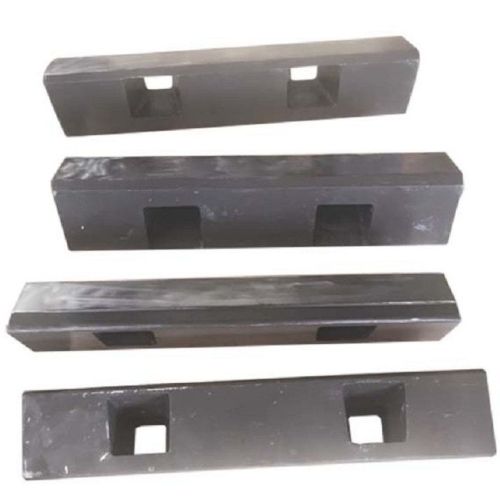
Jaw crusher jaw plate clamping wedges
Clamp jaw plates to the swing or fixed jaw support face. Check jaw plate version, wedge angle, contact, bolts, wear and assembly/removal space.
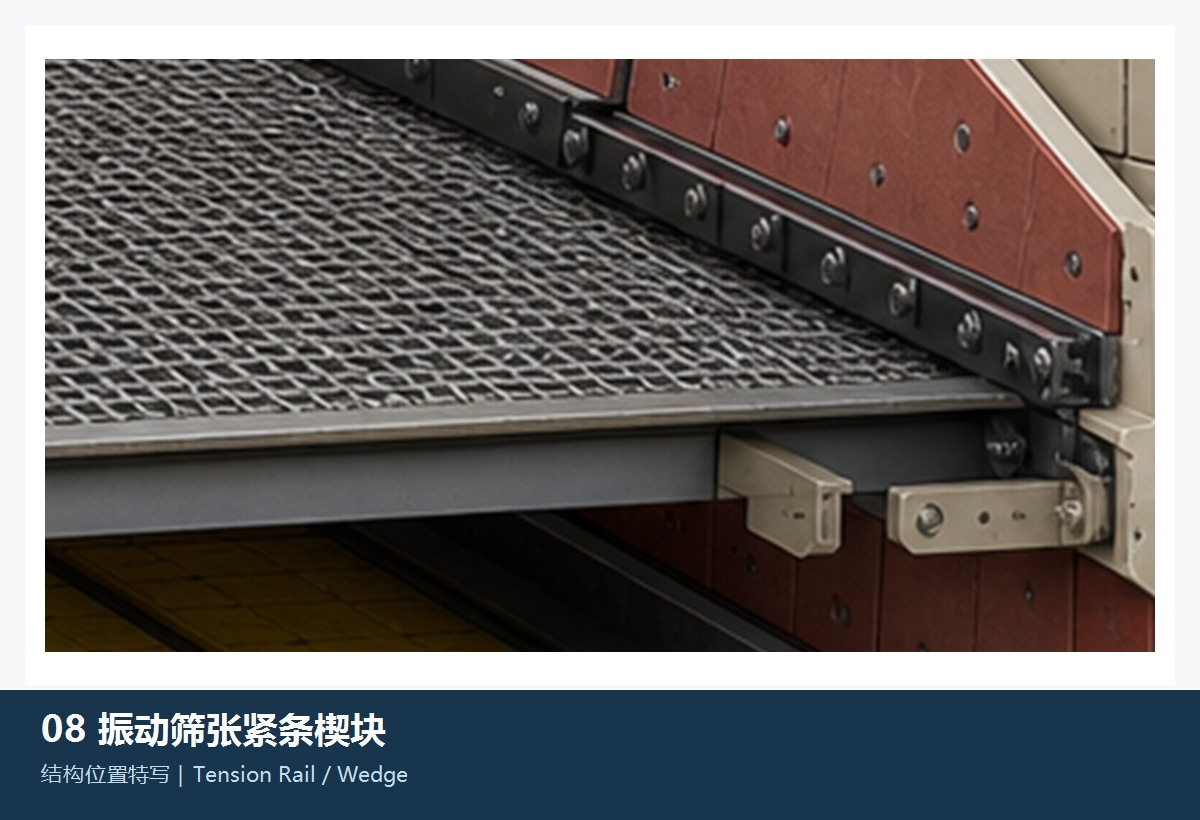
Vibrating screen tension rails and wedges
Apply and maintain screen-media tension. Check the screen box, media type, rail length, wedge angle, vibration and periodic retightening requirements.
Materials, surfaces and fits
Balance strength, toughness, fatigue resistance and serviceability
No single strength class or alloy grade is specified as a universal solution for all pins and bolts.
Failure diagnosis
Trace looseness, fractures and bore wear through the connection system
A stronger bolt or harder pin may not solve preload, fit or fatigue problems.
| Symptoms | الفحوصات ذات الأولوية | Associated Risks |
|---|---|---|
| Repeated bolt loosening | Preload, friction, grip length, contact-face settlement, dynamic loads, retightening and locking method | Joint slip, hole wear and fatigue fracture |
| Bolt fracture at threads or fillets | Material and heat treatment, thread roots, preload, uneven loading, stress concentration and corrosion | Detached components, impacts on adjacent parts and downtime |
| Uneven pin wear | Housing bore coaxiality, bushing clearance, uneven loading, oscillation angle, lubrication and retention | Increased clearance, impact and structural deformation |
| Pin surface spalling or seizure | Surface hardness, hardened layer, roughness, bushing material, bearing pressure and lubrication | Seizure of mating surfaces and damage to bores or housings |
| Locknut loosening or galling | Threads, thread hand, preload, lubrication, locking, contamination and assembly/removal temperature | Loose liners or main shaft thread damage |
| Wedge or clamp displacement | Wedge angle, contact, fastening, support-face wear, vibration and assembly orientation | Loose or displaced liners and support-face damage |
Enquiries and quality control
Information for pin and special fastener supply
Prioritise joint assembly drawings, installation procedures and the failure location on used parts.
المعدات and joint
OEM, complete model, serial number, installation position, assembly number, part number and joint function.
Threads and clamping
Threads, head form, grip length, seating face, holes, nuts and washers, preload and lubrication condition.
Pins and bushings
Shaft diameter, length, steps, holes, bushings, clearance, retention, oscillation angle, bearing pressure and lubrication.
Loads and environment
Tension, shear, bending, impact, fatigue, vibration, temperature, abrasive particles and corrosion.
المواد والتصنيع
Material, heat treatment, surface strengthening, threading process, hardness gradient, non-destructive testing and repair restrictions.
Installation and acceptance
Torque, tensioning or elongation, tools, calibration, retightening, dimensions, properties, batches and traceability.
Technical references: Metso distinguishes static bolts, fatigue-loaded rotating bolts and liner bolts for large mills, treating nuts, washers, spacers, lubrication, torque tools and elongation measurement as one hardware system. Nord-Lock technical guidance explains that insufficient preload can cause loosening, fatigue and joint slip, while excessive preload can damage bolts or connected components.Metso Specialized Hardware · Nord-Lock Bolt Preload
الأجزاء والمعدات ذات الصلة
Related equipment, OEM models, fastener products and materials
المعدات pages explain joint function, OEM pages identify models and drawing references, and product pages cover materials, preload, fits and failure information.
Ball and SAG mills Shell flanges, rotating bodies, liner bolts and complete preload hardware sets.
الكسارات الدوارة والمخروطية Head nuts, locknuts, washers and liner clamping. Impact and hammer crushers Hammer shafts, pivot pins, liner bolts and clamps. Bearings and bushings Pin contact systems, housing bores, lubrication and sealing. العلامات التجارية والموديلات الأصلية Identify dedicated hardware by complete model, assembly number and part number.
Request a quotation for heavy-duty pins and special fasteners
Submit equipment models, assembly and part numbers, joint drawings, preload or fit requirements, materials, loads and failure information for technical review.
خدمات صنع في الصين
من التقييم الفني إلى تسليم المنتج بالكامل
توفر شركة ANRANST للعملاء العالميين تقييمات هندسية، واختيار التصنيع الصيني، ومراقبة الجودة، وتسليم الأجزاء النهائية لقطع الغيار الصناعية المقاومة للتآكل حسب الطلب، ويمكنها أيضًا دعم قطع الغيار الصناعية الأخرى حسب الطلب.
مراجعة الرسومات والهندسة
قم بمراجعة أسطح التزاوج وأبعاد الواجهة، وقم بتقييم جدوى المواد والمعالجة الحرارية والتصنيع.
تحديد المادة والمعالجة الحرارية
تُحدَّد درجات المواد وعمليات المعالجة الحرارية لكل طلب على حدة، وتُثبَّت في الاتفاقية الفنية وتُتابَع أثناء الإنتاج.
ضبط الجودة
يشمل ذلك تأكيد الرسم، ومراقبة المواد والعمليات، وتتبع الإنتاج، وتنسيق عمليات الفحص والقبول.
تسليم المنتج النهائي
تنظيم عمليات التصنيع والتحقق من الجودة والتعبئة والتغليف وتسليم المنتجات النهائية الكاملة لتشكيل حلقة إمداد قابلة للتنفيذ.
قم بتزويدنا بالنماذج الحالية، والرسومات، وأرقام الرسومات، وأرقام الأجزاء، والمواد، أو معلومات ظروف التشغيل، وسنقوم بتحديد التحقق الفني ومسار التوريد وفقًا لذلك.
إرسال طلب