
Drawing and Engineering Review
We review mating surfaces and interface dimensions and assess material, heat treatment and manufacturing feasibility.
Locks the adjustment ring or bowl after setting, preventing rotation and discharge setting drift during operation.
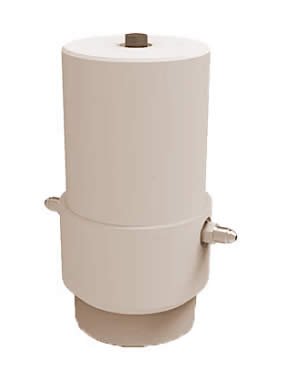
Locking Cylinder Assembly (Clamping Cylinder Assembly)— Cone Crushers Wear part, position 16.
| Installation Position | At the circumferential locking positions around the adjustment ring, labelled Clamping Cylinder in FLS section A. |
| Main Function | Locks the adjustment ring or bowl after setting, preventing rotation and discharge setting drift during operation. |
| Replacement Frequency | Low replacement frequency for the assembly and medium for seals. Service for pressure loss, external or internal leakage, cylinder damage or unsynchronised operation. |
| Item | Details |
|---|---|
| Material Options | Quenched and tempered alloy steel cylinder body and piston, wear-resistant guides and matching seals such as NBR/HNBR/PU |
| Typical Properties and Acceptance Criteria | Specify cylinder strength, bore finish, piston rod surface, seal extrusion clearance, pressure retention and contamination resistance for the maximum system pressure and duty cycles. Acceptance checks include material traceability, dimensions, NDT, pressure and leakage tests, and seal kit identification. A locknut and a clamping cylinder are different spare parts. |
| Principal Failure Mechanism | Abrasion, fatigue, corrosion or assembly damage; use photographs of failed parts from the site to identify the dominant mechanism |
Use these links for preliminary selection. Confirm the complete model, serial or drawing number, drawing revision, dimensions and actual operating conditions to establish fit.
Independent aftermarket information. OEM names and trademarks belong to their respective owners and do not imply authorization, affiliation or endorsement. Confirm the series, complete model, serial or drawing number, drawings and operating conditions before manufacture.
Provide the machine model, operating conditions and target service life so our engineers can recommend materials and prepare a quotation.
Or contact us directly: +86 156 3797 3199
zzx@anranst.com
ANRANST provides customers worldwide with engineering assessment, production at certified foundries to drawing, quality control and finished-part delivery for custom wear parts and industrial spares, with scope to support other custom industrial parts.
We review mating surfaces and interface dimensions and assess material, heat treatment and manufacturing feasibility.
Material grades and heat-treatment processes are specified order by order, confirmed in the technical agreement and tracked through production.
Drawing confirmation, material and process control, production tracking, inspection and acceptance coordination.
We coordinate manufacturing, quality confirmation, packaging and delivery of complete finished parts in a workable, closed-loop supply process.
Provide the existing model, drawings, drawing or part numbers, materials or operating conditions so we can identify the appropriate technical review and supply route.
Submit an Enquiry