01
Grinding Ring
- Technical Requirements
- Working surface: approximately 58-65 HRC, depending on material and heat treatment. Control carbide distribution, cracking and roundness.
Ring roller mills produce fine powders by rolling grinding rollers against a grinding ring. Applications include ground calcium carbonate, talc, barite and limestone. The diagrams below show part locations in a multi-level ring roller arrangement; confirm the number of levels, part dimensions and materials for the actual model.
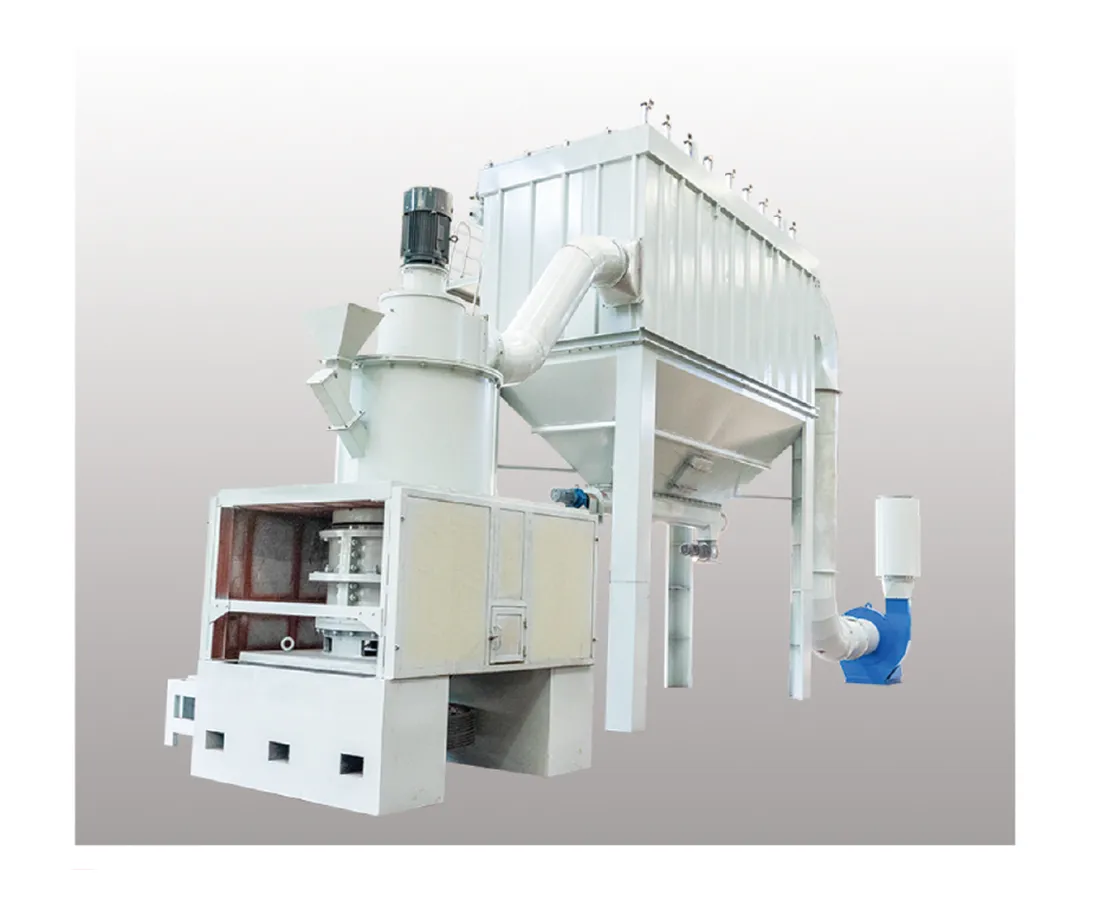
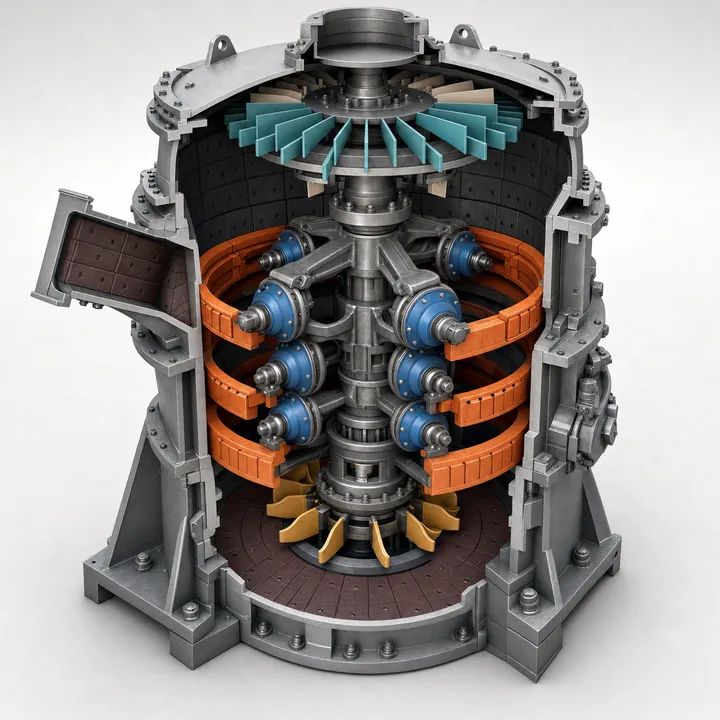
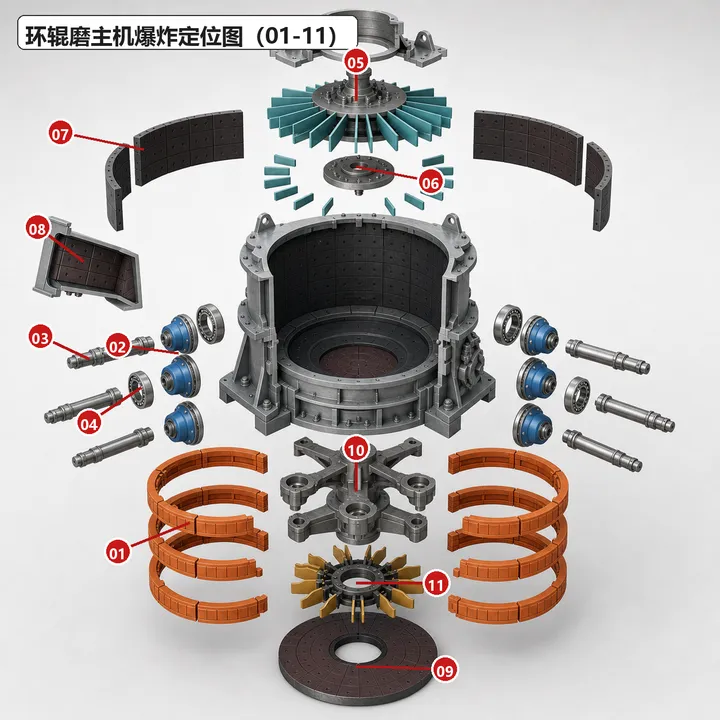
Ring roller mills produce fine powders by rolling grinding rollers against a grinding ring. Applications include ground calcium carbonate, talc, barite and limestone. The diagrams below show part locations in a multi-level ring roller arrangement; confirm the number of levels, part dimensions and materials for the actual model.
Explore part names, images, material options and technical requirements. Select a card to open the corresponding replacement part page.
Grinding Ring
Grinding Roller
Grinding roller shaft / mainshaft
Grinding Roller Bearing
Classifier Wheel
Classifier Blade
Housing Liners
Feed Chute Liner
Bottom Plate Liner
Roller Carrier / Spider
Material Plough / Plough Blade
Materials for similarly named parts may differ by OEM, machine model and operating conditions. Confirm the machine model, OEM drawing number and measured dimensions before ordering or manufacture.
Provide the machine model, operating conditions and target service life so our engineers can recommend materials and prepare a quotation.
Or contact us directly: +86 156 3797 3199
zzx@anranst.com
Browse component descriptions, drawing requirements and enquiry details.
ANRANST provides customers worldwide with engineering assessment, production at certified foundries to drawing, quality control and finished-part delivery for custom wear parts and industrial spares, with scope to support other custom industrial parts.
We review mating surfaces and interface dimensions and assess material, heat treatment and manufacturing feasibility.
Material grades and heat-treatment processes are specified order by order, confirmed in the technical agreement and tracked through production.
Drawing confirmation, material and process control, production tracking, inspection and acceptance coordination.
We coordinate manufacturing, quality confirmation, packaging and delivery of complete finished parts in a workable, closed-loop supply process.
Provide the existing model, drawings, drawing or part numbers, materials or operating conditions so we can identify the appropriate technical review and supply route.
Submit an Enquiry